 精密フライスカッター,あらゆる材料を加工するCNC用の切削工具
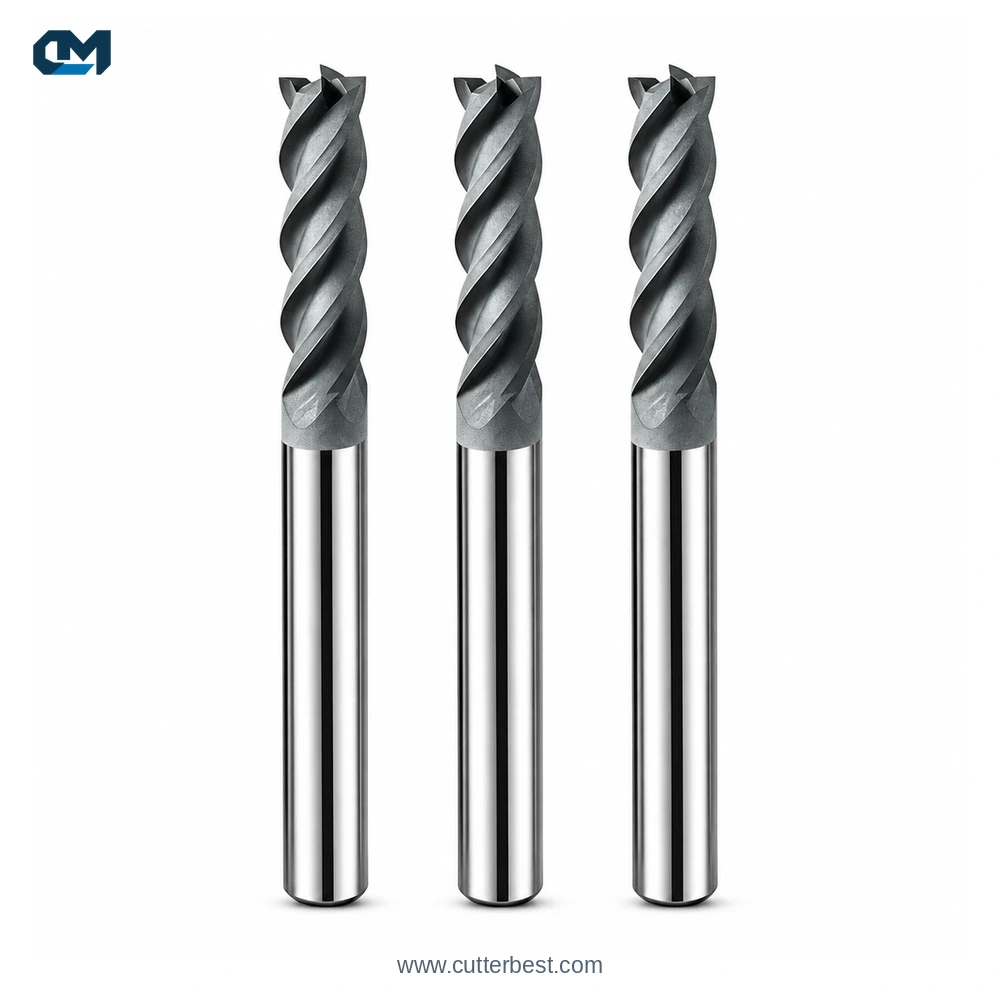
Standard Sizes for Diamond Coated Square End Mills
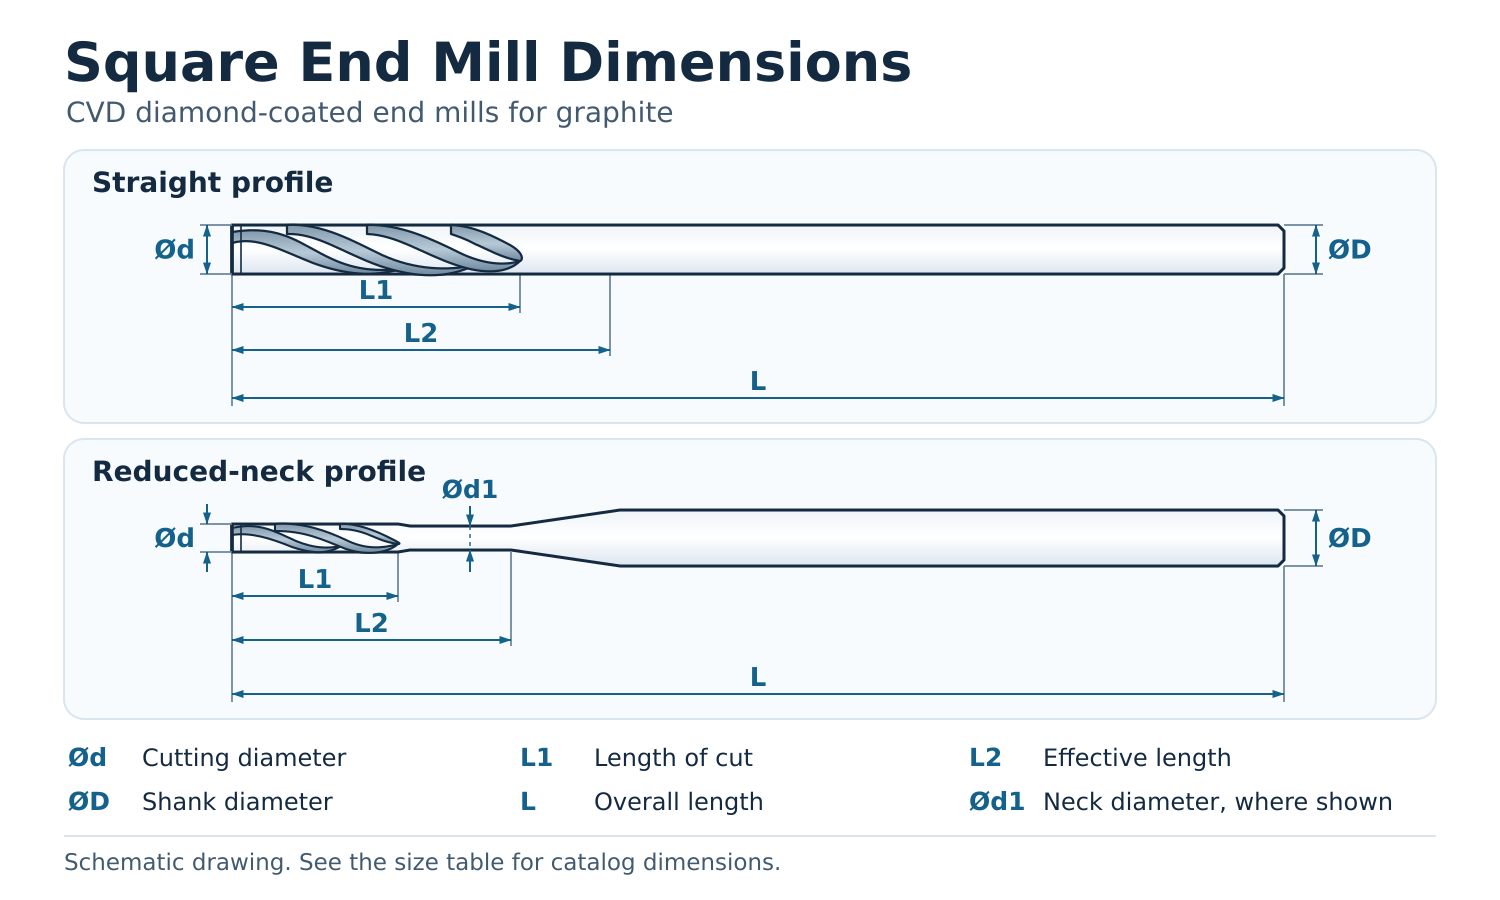
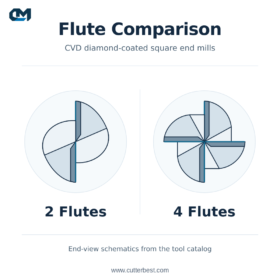
Start with the cutting diameter you need for graphite machining. These diamond coated square end mills come in specific catalog combinations of length of cut, 有効長さ, 全長, シャンク径, そしてフルートの番手. Confirm the full configuration before ordering. すべての寸法は mm 単位です.
| Cutting Diameter d | Length of Cut L1 | Effective Length L2 | Overall Length L | Shank Diameter D | フルート |
|---|---|---|---|---|---|
| 0.2 | 0.4 | 2 | 50 | 4 | 2 |
| 0.3 | 0.6 | 3 | 50 | 4 | 2 |
| 0.4 | 0.8 | 4 | 50 | 4 | 2 |
| 0.5 | 1 | 6, 10 | 50 | 4 | 2 |
| 0.6 | 1.2 | 6, 10 | 50 | 4 | 2 |
| 0.8 | 2 | 6, 10 | 50 | 4 | 2 |
| 1† | 3 | 6, 10, 15, — | 50, 60, 75 | 4 | 2, 4 |
| 1.5† | 4 | 6, 10, 15 | 50, 60, 75 | 4 | 2, 4 |
| 2† | 6 | 10, 15, 20, — | 50, 60, 75 | 4 | 2, 4 |
| 3† | 10, 15 | 15, — | 50, 60, 75, 100 | 3, 4 | 4 |
| 4 | 12, 20 | — | 50, 60, 75, 100 | 4 | 4 |
| 6 | 20, 25, 30, 40 | — | 50, 60, 75, 100, 150 | 6 | 4 |
| 8 | 20, 30, 40 | — | 50, 60, 75, 100, 150 | 8 | 4 |
| 10 | 25, 30, 50 | — | 60, 75, 100, 150 | 10 | 4 |
| 12 | 40, 50 | — | 100, 150, 180 | 12 | 4 |
† For the marked diameters, check the exact combination of lengths, シャンク径, そしてフルートの番手. The Ø3 mm tool with a 15 mm length of cut has a 100 mm overall length and a Ø3 mm shank.
A dash (—) means the catalog gives no separate L2 value for one or more configurations at that diameter.
Square End Mills for Graphite Machining
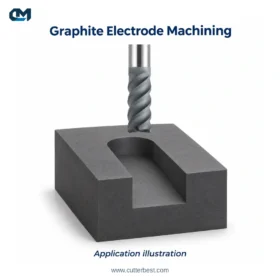
Square end mills are used to mill flat-bottom slots in graphite electrodes and to machine pocket floors and straight sidewalls in graphite mold components. For narrow features, the catalog lists two-flute tools at Ø0.2, Ø0.3, Ø0.4, Ø0.5, Ø0.6, and Ø0.8 mm. Check the cutting diameter and effective length against your part drawing.
Dimensions and Drawing
| シンボル | 寸法 |
|---|---|
| d | Cutting diameter across the cutting edges |
| L1 | Length of cut measured along the tool axis from the tip to the end of the cutting edges |
| L2 | Effective length measured along the tool axis from the tip to the L2 reference line on the drawing |
| L | Overall length from the tool tip to the end of the shank |
| D | Shank diameter at the clamping section |
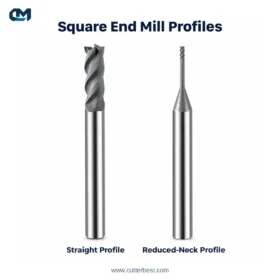
| d1 | Neck diameter where shown on the drawing |
Use L2 as a tool dimension when checking reach. Maximum machining depth depends on clearance between the workpiece, ネック, シャンク, and holder in your setup. If neck clearance is critical, request the drawing for the selected configuration to confirm d1.
Selecting a Standard Configuration
- Match the cutting diameter and length of cut to the feature. Start with the slot width or pocket geometry. Check that L1 provides the cutting edge length needed for the operation.
- Compare effective lengths for recessed features. Both Ø0.5 mm configurations have a 1 切断長さ mm. Their effective lengths are 6 mmと 10 ミリメートル.
- Check the holder fit. The catalog lists two four-flute Ø3 mm configurations with a 10 mmの切断長さとa 50 全長mm. One has a Ø3 mm shank and the other has a Ø4 mm shank.
For other workpiece materials, see our general-purpose flat end mills.
CVD Coating and Supply
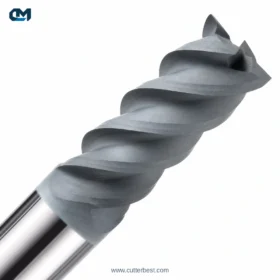
CVD ダイヤモンドコーティングは、グラファイトのフライス加工時の摩耗に耐えます。. We supply standard catalog sizes and review drawings for custom diamond-coated square end mills. For other end geometries, see our CVDダイヤモンドコーティングエンドミルシリーズ.
Related Technical Guides
- Compare square end, ボールノーズ, and corner radius geometries in our ダイヤモンドコーティングエンドミルの選定ガイド.
- For graphite electrodes, 金型キャビティ, and recessed features, のガイドを参照してください グラファイト荒加工および仕上げ加工用エンドミルの選択.
見積もりを依頼する
- Standard sizes. Send the required cutting diameter and quantity. Include any specified length of cut, 有効長さ, 全長, シャンク径, そしてフルートの番手. We’ll confirm the catalog configuration before quoting.
- Custom tools. 図面を送信する, スケッチ, or key dimensions, along with the graphite feature to be machined and the quantity. For recessed features, include the required reach and any clearance limits.
If you have only partial dimensions, send what you have so we can start the review.
電子メール sales@cutterbest.com 又は send your requirements on WhatsApp for a quote.