 精密フライスカッター,あらゆる材料を加工するCNC用の切削工具

Learning how to choose diamond coated end mills is important when machining graphite, CFRP, GFRP, 高シリコンアルミニウム, およびその他の研磨性の非鉄材料. The wrong flute design, 工具の長さ, エンドタイプ, or cutting condition can still cause fast wear, 表面仕上げが悪い, エッジダメージ, or unstable dimensions.
This is especially true in abrasive and non-ferrous machining. These materials wear ordinary carbide tools quickly, but they do not all need the same cutter design.
このため, buyers and engineers should start with the workpiece material and machining operation. Then they can compare flute design, 切断径, 工具の長さ, エンドタイプ, coating quality, 工具剛性, and custom requirements.
If you need standard or custom tools for graphite and CFRP machining, あなたは私たちをチェックすることができます ダイヤモンドコーティングエンドミル.
This guide explains how to choose a suitable diamond coated end mill for graphite electrodes, グラファイトモールド, CFRPトリミング, GFRP milling, 高シリコンアルミニウム, and custom non-ferrous machining projects.
クイックセレクションガイド: ダイヤモンドコーティングエンドミルの選び方
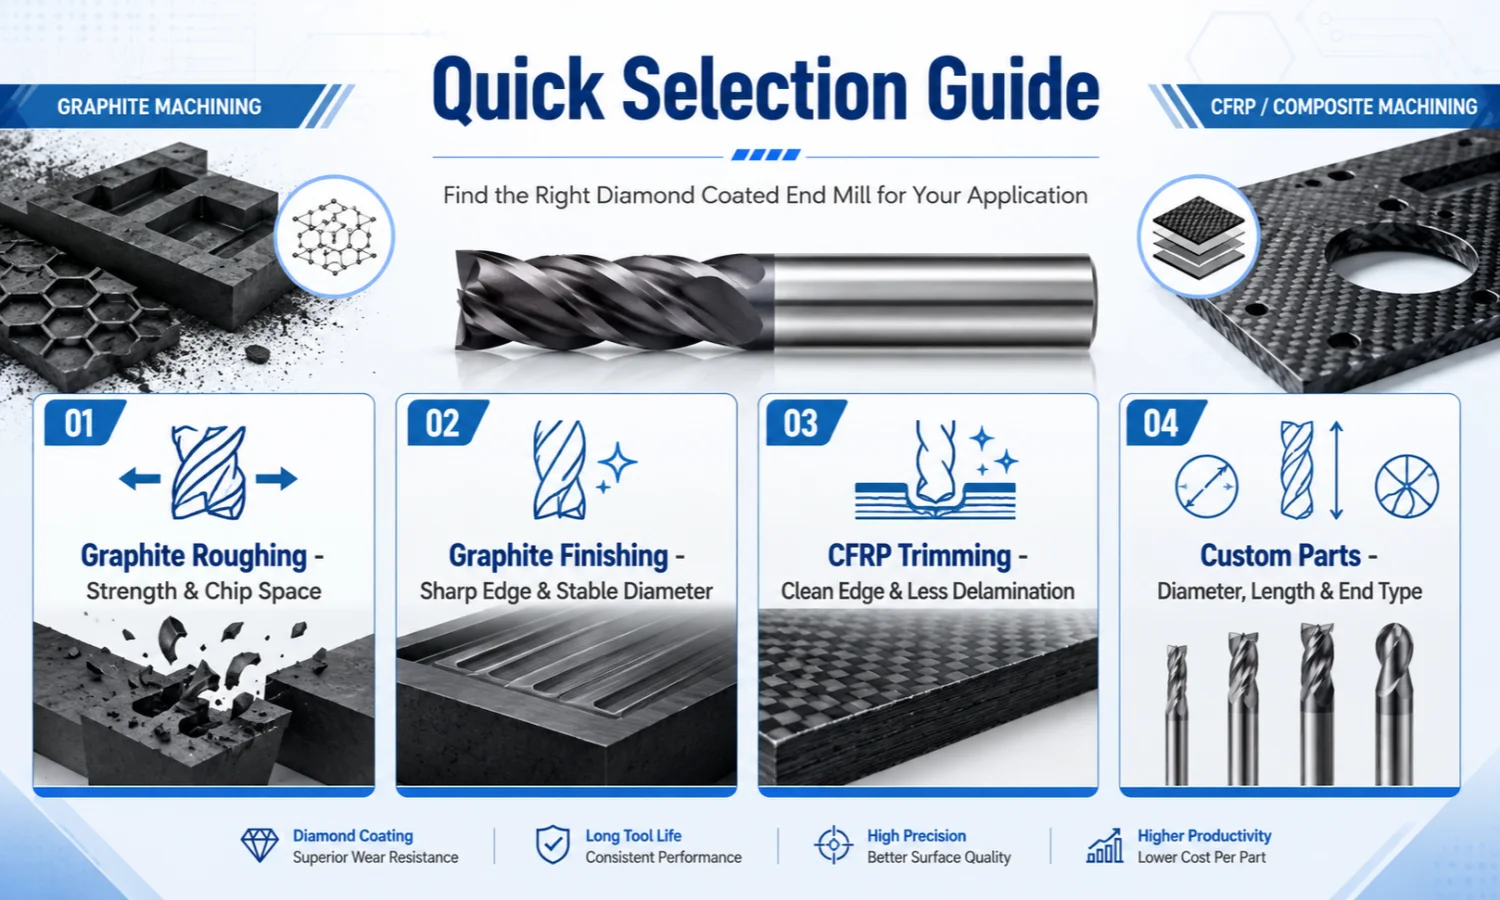
Before reviewing each detail, you can use this table as a quick starting point. テストカットの代わりにはなりません, but it helps narrow down the tool direction.
| 機械加工の必要性 | 推奨されるツールの焦点 | Practical Selection Note |
|---|---|---|
| グラファイト粗加工 | Strong tool body, enough chip space | Choose a rigid tool and avoid unnecessary long flute length |
| グラファイト仕上げ | Sharp edge, stable diameter, good repeatability | Focus on surface finish and dimensional stability |
| グラファイト電極のミリング | Wear resistance and stable cutting geometry | Suitable for fine details, 空洞, and long cutting cycles |
| CFRPトリミング | Clean cutting edge and suitable flute geometry | 毛羽立ちの軽減に役立ちます, ファイバーの引き出し, 剥離 |
| GFRP milling | Strong coating and stable geometry | Helps control wear in abrasive composite materials |
| ハイシリコンアルミニウムのフライス加工 | Diamond coating and suitable flute design | Helps improve tool life in abrasive non-ferrous machining |
| Deep cavities or special parts | カスタム直径, 首の長さ, 刃の長さ, and end type | Use drawing-based production when standard tools cannot reach or stay rigid |
ステップ 1: ワーク材質の確認
Workpiece material is the first decision point. A diamond coated tool may perform very well in one material, but it may not be suitable for another.
黒鉛
グラファイト加工では, wear resistance and diameter stability are critical. Graphite is not hard like steel, しかし、それは研磨性があり、埃っぽいです. As the cutting edge wears, the tool diameter may change, and this can affect electrode details, 金型キャビティ, and fine contours.
黒鉛荒加工用, start with a rigid tool body, 安定したクランプ, and enough chip space. グラファイト仕上げ用, give more attention to edge sharpness, tool diameter stability, surface finish, と再現性.
In most graphite electrode and graphite mold applications, the key question is not only “Can the tool cut graphite?” The better question is: “Can the tool keep the same cutting quality after a long cutting cycle?」
CFRPとGFRP
CFRP and GFRP create a different problem. The tool must cut fibers and resin cleanly. If the edge becomes dull or the geometry does not match the laminate structure, the part may show fuzzing, ファイバーの引き出し, rough edges, or delamination.
For composite trimming, the cutter should not only resist wear. It should also support clean edge quality. したがって, フルートの形状, エッジの状態, 機械剛性, and dust removal all matter.
ハイシリコンアルミニウム
High-silicon aluminum is more abrasive than common aluminum. In this type of non-ferrous machining, diamond coated tools may help improve tool life and cutting stability.
しかし, the final choice still depends on silicon content, 部品形状, 機械の状態, 表面仕上げ要件, and production volume.
Materials Not Recommended: スチールとステンレススチール
Diamond coated end mills are usually not the first choice for steel, ステンレス鋼, チタン, または他の鉄材料. These materials often need carbide end mills with coatings designed for heat resistance and cutting toughness.
鋼用, ステンレス鋼, and other ferrous materials, you can compare our 超硬エンドミルカッター options here.
ステップ 2: Match the Tool to the Machining Operation
The same cutter may not work equally well for roughing, 仕上げ, trimming, スロッティング, および輪郭フライス加工. したがって, choose the tool based on the operation, not only by diameter.
Graphite Roughing
Graphite roughing focuses on material removal and stable cutting. The tool needs enough strength and chip space. If the flute space is too limited, dust and chips may affect cutting stability.
A practical starting point is to choose the shortest tool that can safely reach the machining area. This helps improve rigidity and reduce vibration.
Graphite Finishing
Graphite finishing needs a sharper edge and stable tool diameter. 放電加工電極加工において, small details, sharp corners, 肋骨, and cavity features can affect the final mold result.
このため, graphite finishing endmills should focus on edge quality, dimensional stability, そして表面仕上げ. A worn edge can reduce detail accuracy even when the tool still looks usable.
CFRP Trimming
CFRP trimming needs clean cutting rather than heavy material removal. If the edge quality is poor, the workpiece may show fuzzing, delamination, or fiber pull-out.
A suitable diamond coated end mill for CFRP should combine wear resistance with a cutting geometry that supports clean trimming. 加えて, stable fixturing and dust removal are important.
Slotting and Contour Milling
Slotting and contour milling need a balance between chip evacuation, 工具の強度, そして表面品質. If the slot is deep or the contour is thin, tool rigidity becomes more important.
In these cases, do not choose the longest flute length by default. その代わり, match flute length to the actual cutting depth.
Custom Graphite or Composite Parts
Some graphite molds, composite components, 深い空洞, or thin-wall parts need custom tool geometry. Standard tools may not provide enough reach, 剛性, or edge quality.
非標準要件の場合, あなたは私たちを確認することができます カスタムエンドミル.
ステップ 3: Choose the Right Flute Design
Flute design affects chip evacuation, 切削安定性, そして表面仕上げ. It also affects how the tool behaves in graphite dust or composite fibers.
Lower Flute Counts
Lower flute counts usually provide more chip space. They may work better for roughing or for operations where chip evacuation is important.
黒鉛荒加工用, this can help maintain cutting stability. しかし, the best choice still depends on tool diameter, 切込み深さ, 機械剛性, and the required surface finish.
Higher Flute Counts
Higher flute counts may support smoother finishing in some applications. They can also help improve surface consistency when the machine setup is stable.
しかし, more flutes are not always better. If chip space becomes too small, the tool may rub, heat may increase, and cutting stability may decline.
Composite-Specific Geometry
For CFRP and GFRP, flute design should support clean fiber cutting. A general end mill may cut the shape, but it may leave fuzzing or rough edges if the geometry does not match the composite material.
When edge quality is critical, the tool design should be selected around trimming quality, laminate structure, and production stability.
Custom Flute Geometry
For non-standard graphite parts or composite components, custom flute geometry may provide better results than standard tools. This is especially useful for long reach tools, 深い空洞, 特別なプロファイル, or strict edge requirements.
The goal is not to customize every tool, but to solve reach, 剛性, エッジ品質, or profile problems that standard tools cannot handle.
ステップ 4: Select the End Type
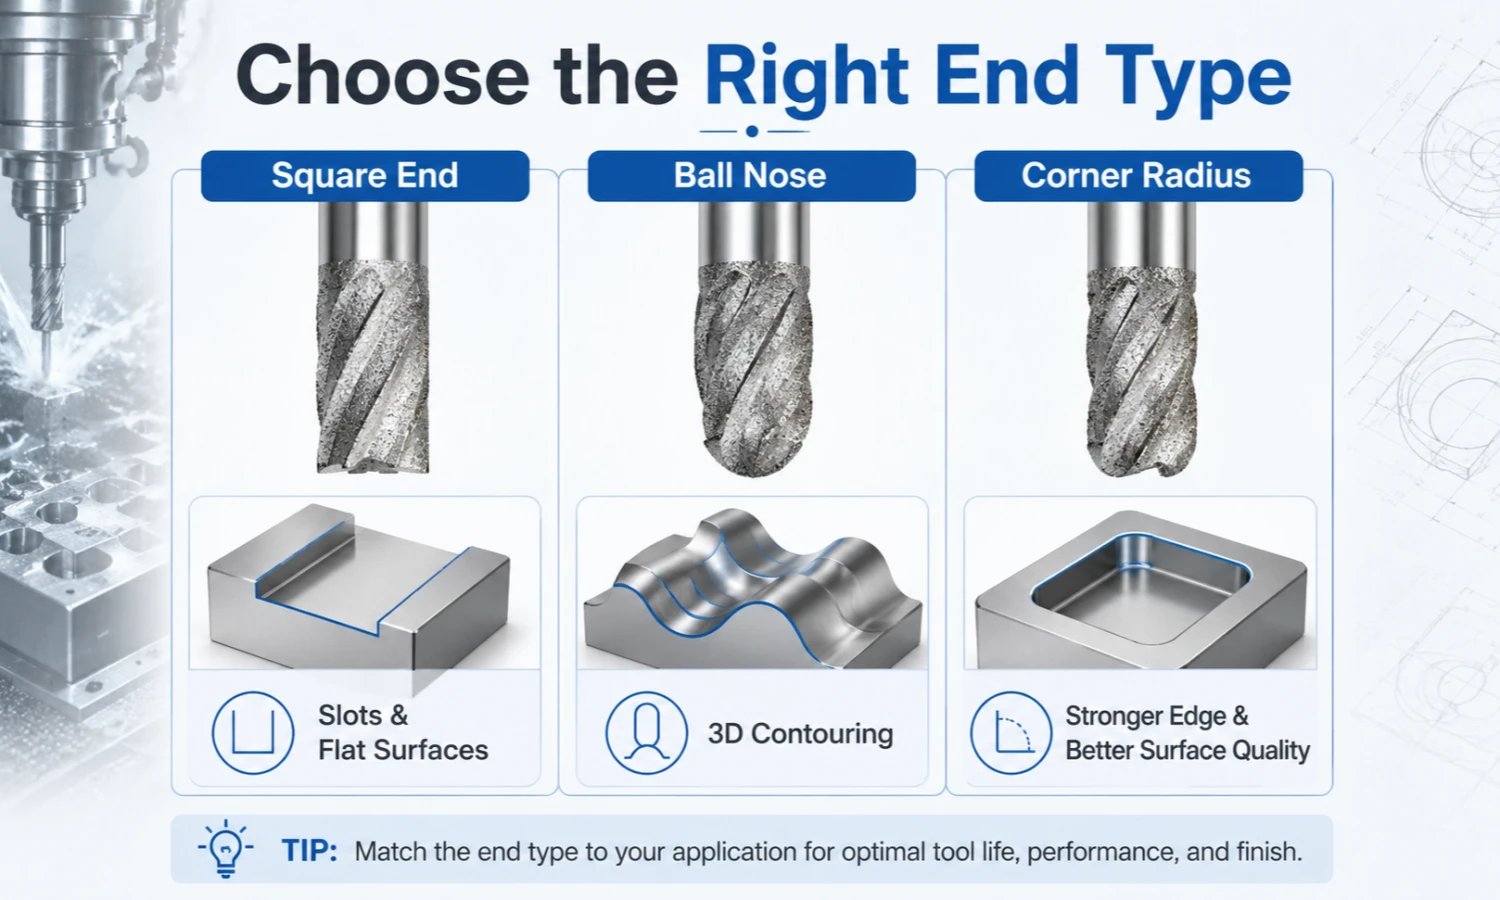
The end type should match the shape of the part and the machining purpose. スクエアエンド, ボールノーズ, and corner radius tools solve different machining needs.
スクエアエンド
Square end tools work well for slots, 平面, 側面フライス加工, and general graphite or composite machining. They create flat-bottom features and straight side walls.
Choose this type when the part needs clean shoulders, 平面, or standard milling features.
ボールノーズ
Ball nose tools are suitable for 3D contouring, 曲面, および金型関連の機械加工. They help create smoother tool paths on complex shapes.
For graphite molds, electrodes, および 3D プロファイル, a ball nose diamond coated end mill may be more suitable than a square end tool.
コーナー半径
Corner radius tools offer better edge strength than sharp square end tools. They may be useful when the application needs both tool strength and better surface quality.
This design can help reduce corner chipping and improve stability in some graphite and non-ferrous machining conditions.
ステップ 5: Check Cutting Diameter, Flute Length and Tool Length
Tool size affects machining stability. A very long tool may vibrate more easily, while a very short tool may not reach the required area.
For graphite and composite machining, this is especially important because vibration can reduce edge quality and speed up tool wear.
| Tool Detail | What to Confirm | Practical Selection Tip |
|---|---|---|
| 切断径 | スロット, 輪郭, or feature size | Match the part geometry and required detail |
| 刃長さ | Actual cutting depth | Avoid unnecessary flute length when rigidity matters |
| 全長 | Machine setup and workpiece height | Use only the reach needed for the job |
| 首の長さ | Deep cavities or complex parts | Helps avoid interference in deep machining |
| シャンク径 | Tool holder and machine requirement | Supports stable clamping and lower runout |
| 工具オーバーハング | Distance from holder to cutting area | Keep it as short as possible for better rigidity |
A common mistake is choosing a longer tool “just in case.” In practice, unnecessary length can increase vibration and reduce tool life. When the required reach is uncertain, start with the shortest tool that can safely complete the operation.
If the part has deep cavities, 薄い壁, or special contours, prepare a drawing or sample photo before requesting a recommendation.
ステップ 6: Understand Coating Quality and Tool Structure
Diamond coating matters, but coating alone does not decide tool performance. This is why choosing diamond coated end mills should include coating quality, carbide substrate, エッジの準備, and tool geometry together.
ダイヤモンドコーティング
Diamond coating helps improve wear resistance when machining abrasive materials. This is why many manufacturers choose diamond coated tools for graphite electrodes, CFRPトリミング, GFRP milling, and high-wear non-ferrous applications.
しかし, tool life is not decided by coating only. 材質グレード, 工具形状, 機械剛性, 切削条件, and clamping quality also affect the final result.
Carbide Substrate and Edge Preparation
A stable carbide substrate supports tool rigidity and cutting strength. その間, edge preparation affects sharpness, strength, そして表面品質.
For graphite finishing and CFRP trimming, the cutting edge should stay sharp enough to maintain clean cutting. For roughing or stronger cutting loads, edge strength may become more important.
Diamond Coated vs PCD vs DLC
Different diamond-related tool solutions do not work the same way. The table below gives a simple comparison for purchasing and selection discussions.
| 道具 / コーティングの種類 | Basic Structure | Typical Strength | 選択メモ |
|---|---|---|---|
| Diamond coated end mill | Carbide substrate with diamond coating | Wear resistance in abrasive non-ferrous materials | Common choice for graphite, CFRP, GFRP, そして高シリコンアルミニウム |
| PCD tool | Polycrystalline diamond cutting edge | Strong wear resistance in selected non-ferrous applications | Often considered for stable, high-volume production |
| DLC coated tool | Carbon-based coating on the tool surface | Lower friction in some non-ferrous applications | Different from diamond coating; suitability depends on material and operation |
If the application is not clear, do not choose by coating name only. First confirm the material, 手術, surface requirement, and production volume.
ステップ 7: Check Cutting Conditions Before Machining
Even the right tool can perform poorly if the cutting condition is not suitable. 生産前, review the machine setup, クランプ, 工具振れ, 防塵, そしてカット戦略.
Spindle Speed and Feed Rate
Spindle speed and feed rate should match the tool diameter, 材料, および機械加工作業. If the feed is too low, the tool may rub instead of cutting. If the feed is too aggressive, the cutting edge may wear or become unstable.
したがって, test cutting is useful before batch production, especially for custom graphite parts or composite trimming.
Depth of Cut and Tool Rigidity
Depth of cut should match tool length, workpiece shape, と機械剛性. A long overhang can increase vibration, especially in deep cavities or thin-wall parts.
When rigidity is limited, a shorter flute length, stronger neck design, or adjusted cutting strategy may improve stability.
Dust Control, Cooling and Runout
Graphite machining creates dust, so dust control and air evacuation are important. Composite machining also needs stable cutting and clean edges.
どちらの場合も, tool runout can affect surface finish, エッジ品質, と工具寿命. 生産前, check the tool holder, clamping condition, なくなる, とマシンの安定性.
| Cutting Condition | 確認すべきこと | What Can Go Wrong If Ignored |
|---|---|---|
| 主軸速度 | Match tool diameter and material | 熱, こする, または切断が不安定 |
| 送り速度 | Avoid rubbing or overly aggressive cutting | Fast wear, poor surface, or edge damage |
| Depth of cut | Match tool length and rigidity | Vibration and reduced tool life |
| Dust control | Remove graphite dust effectively | Poor visibility, 不安定な切断, or contamination |
| 工具振れ | Check holder and clamping | Poor finish and uneven edge wear |
| ワークホールディング | Keep the part stable | おしゃべり, delamination, or dimensional error |
This table is a starting checklist. Final parameters should be confirmed through material condition, マシンの能力, and test cutting.
ステップ 8: Avoid Using the Wrong Tool for the Material
Before choosing a diamond coated end mill, confirm whether the material is suitable for diamond coating. These tools mainly support graphite, CFRP, GFRP, 高シリコンアルミニウム, 研磨性の非鉄材料.
They are usually not the best choice for steel, ステンレス鋼, チタン, または他の鉄材料. If the material is wrong, 工具寿命, surface finish, and cutting stability may all become worse.
For a basic explanation of applications, you can also read our guide on what diamond coated end mills are used for.
ステップ 9: Decide Whether You Need Standard or Custom Tools
Standard tools can work for many common machining jobs. しかし, custom tools may fit deep cavities, 細かい部分, special edge requirements, or non-standard dimensions better.
When Standard Tools May Work
Standard tools may be suitable when the material, 切込み深さ, 工具サイズ, and machining operation are common. 例えば, standard diamond coated end mills can support many graphite electrode, 型, and composite trimming applications.
If the part does not need special reach, special profile, or unusual dimensions, a standard size may be enough.
When Custom Tools Are Better
You may need custom diamond coated end mills if your project requires:
- Special cutting diameter
- Longer flute length
- Longer overall length
- Special neck design
- スクエアエンド, ボールノーズ, or corner radius design
- Drawing-based tool production
- OEM or ODM requirements
- Special marking or packaging
As a practical rule, custom tools become more useful when reach, 剛性, エッジ品質, or part geometry cannot be solved by a standard catalog size.
より広範なグラファイトフライス加工用途向け, 私たちのレビューもできます ダイアモンドミーリングカッター for graphite machining:
What Information Should You Send for a Quotation?
To get an accurate quotation, send complete tool and machining information. This helps reduce misunderstanding and makes the recommendation more practical.
| 必要な情報 | 例 |
|---|---|
| ワーク材質 | 黒鉛, CFRP, GFRP, 高シリコンアルミニウム |
| 機械加工作業 | 荒加工, 仕上げ, trimming, スロッティング |
| 切断径 | 標準サイズまたはカスタムサイズ |
| 刃長さ | According to cutting depth |
| 全長 | According to machine setup |
| エンドタイプ | スクエアエンド, ボールノーズ, コーナー半径 |
| 機械の状態 | Spindle speed range, ツールホルダー, machine rigidity if available |
| 量 | お試し注文または一括注文 |
| 図面またはサンプル | カスタムツールに推奨 |
The more details you provide, the easier it is to select the right tool. カスタムツールの場合, drawings or sample photos are especially helpful.
Common Mistakes When Choosing Diamond Coated End Mills
Choosing Only by Diameter
直径は重要です, but it is not enough. フルートのデザイン, 切断長さ, コーティング, エンドタイプ, and machining method also affect performance.
正しい直径の工具であっても、溝の長さが, エッジデザイン, またはコーティングの選択が用途に合わない.
荒加工と仕上げ加工に同じ工具を使用する
荒加工と仕上げ加工では、異なる工具設計が必要になることがよくあります. 荒加工ツールは強度と材料の除去に重点を置く必要があります. 仕上げツールは表面の品質と精度に重点を置く必要があります.
したがって, 1 つのツールがすべてのプロセスに最適なオプションであるとは限りません.
ワーク材質を無視する
黒鉛, CFRP, GFRP, と高シリコンアルミニウムは同じように動作しません. すべての用途に 1 つのカッターを使用するのではなく、ツールは材料に適合する必要があります.
これは、グラファイト電極加工と CFRP トリミングを切り替える場合に特に重要です。.
工具長の選択が長すぎる
長いツールの方がリーチが広いため、より安全に見えるかもしれません. しかし, unnecessary length can reduce rigidity and increase vibration.
For graphite and composite machining, poor rigidity can affect tool life, surface finish, and edge quality.
Not Sending Drawings for Custom Tools
カスタムツールの場合, drawings or sample photos help confirm the correct geometry. Without these details, the quotation may not be accurate.
If the part has deep cavities, 薄い壁, special contours, or strict surface requirements, send as much detail as possible.
FAQ
How do I choose diamond coated end mills for graphite?
機械加工作業から始めます, 切断径, 刃の長さ, エンドタイプ, および必要な表面仕上げ. For graphite electrodes and molds, wear resistance and dimensional stability are especially important.
Are diamond coated end mills good for CFRP?
はい. They can support CFRP trimming and milling because the coating helps improve wear resistance. しかし, エッジジオメトリ, 機械剛性, and dust control also affect fuzzing, delamination, and fiber pull-out.
Can I use diamond coated end mills for steel?
鋼やステンレス鋼にはお勧めしません. 鉄系材料用, 通常は、適切なコーティングを施した超硬エンドミルの方が優れた性能を発揮します。.
What flute design is better for graphite machining?
黒鉛荒加工用, a flute design with more chip space may help improve chip evacuation and tool stability. グラファイト仕上げ用, sharp edge quality and stable tool diameter become more important.
Should I choose square end, ボールノーズ, またはコーナー半径?
Choose square end tools for slots, 平面, そしてサイドミーリング. For 3D contouring and curved surfaces, 通常はボールノーズツールの方が適しています. When you need better edge strength and stable surface quality, コーナー半径ツールの方が良い選択肢になる可能性があります.
ダイヤモンドコーティングエンドミルとPCD工具の違いは何ですか?
Diamond coated end mills use a carbide substrate with diamond coating on the cutting surface. PCD ツールは多結晶ダイヤモンド刃先を使用しています. The better option depends on material, 工具サイズ, edge requirement, production volume, そしてコスト目標.
When should I request custom diamond coated end mills?
You may need custom tools for non-standard diameters, より長い刃長, longer overall lengths, special neck designs, special end types, 深い空洞, or drawing-based production.
What information should I send before asking for a quotation?
ワーク素材をお送りください, 機械加工作業, 切断径, 刃の長さ, 全長, エンドタイプ, 量, 可能な場合は図面またはサンプル写真.
結論
Understanding how to choose diamond coated end mills requires more than selecting a diameter from a catalog. You should first confirm the workpiece material, then match the tool to the machining operation, flute design, エンドタイプ, 工具の長さ, coating quality, そして機械の状態.
For graphite electrodes, グラファイトモールド, CFRPトリミング, GFRP milling, and high-silicon aluminum machining, the right tool can help improve wear resistance, 切削安定性, and machining consistency.
と 16 長年の切削工具製造経験, OMIST can help customers review material, 工具サイズ, and machining requirements before production.
Get Support for Diamond Coated End Mills
グラファイト用ダイヤモンドコートエンドミルが必要な場合, CFRP, GFRP, 高シリコンアルミニウム, または他の研磨性の非鉄材料, あなたのワーク材料を私たちに送ってください, 工具サイズ, 描画, 機械加工作業, そして量.
OMIST は、標準ツールかカスタムツールかを確認するのに役立ちます。 ダイヤモンドコーティングエンドミル あなたのプロジェクトにより適しています.