 Präzisions-Fräser,Schneidwerkzeuge für die CNC-Bearbeitung jedes Materials

Understanding how to choose a ball nose end mill can help improve surface finish, Bearbeitungsstabilität, and tool selection accuracy. Jedoch, the correct cutter depends on more than diameter alone.
This guide explains how to select a ball nose end mill according to the workpiece material, Bearbeitungszweck, Fräserdurchmesser, Kugelradius, Flötenzahl, coating or edge treatment, Werkzeugreichweite, Maschinenstabilität, und Anforderungen an die Oberflächenbeschaffenheit.
For available standard and custom carbide cutters, Sehen Sie sich unsere an Hartmetall-Kugelfräser.
Quick Ball Nose End Mill Selection Guide
The table below provides a practical starting point. Final tool selection should also consider the actual part geometry, Werkstückhärte, Bearbeitungstiefe, Maschinenzustand, und Endbearbeitungsanforderung.
| Bearbeitungsanforderung | Auswahlfokus |
|---|---|
| Allgemeine CNC-Bearbeitung | Match the cutter series to the workpiece material and hardness |
| Gehärtete Materialien | Select the appropriate hardened or high-hardness series |
| Graphitelektroden | Use a dedicated graphite tool with CVD diamond coating |
| Deep Cavities | Confirm neck clearance, Werkzeugreichweite, and minimum practical overhang |
| Fine 3D Details | Use a diameter and ball radius that match the feature size |
| 2-Flute or 4-Flute | Choose according to material, Chipraum, Steifigkeit, and finishing requirements |
| High Surface Finish | Control tool reach, Auslaufen, step-over, und Maschinenstabilität |
This table is a starting point rather than a universal specification. The final cutter should match the actual workpiece and machining setup.
Why Choosing the Right Ball Nose End Mill Matters
A ball nose end mill has a fully rounded cutting end that follows slopes, Hohlräume, Radien, und komplexe dreidimensionale Profile.
Jedoch, one cutter cannot suit every machining condition. Werkstückhärte, Fräsergröße, Flötenkonfiguration, Beschichtung, Werkzeugreichweite, and machine stability all affect the final result.
The purpose of tool selection is therefore not simply to choose a diameter. The complete cutter configuration should match the workpiece and machining requirement.
So wählen Sie einen Kugelfräser aus: 7 Key Factors
Vor der Bestellung, confirm these seven factors:
- Werkstückmaterial und Härte
- Machining purpose
- Schnittdurchmesser, Kugelradius, und Werkzeugreichweite
- Flötenzählung
- Coating or edge treatment
- Anforderung an die Oberflächenbeschaffenheit
- Machine and tool-holder stability
Each factor affects the others, so they should be evaluated together.
1. Wählen Sie nach Werkstückmaterial
Workpiece material and hardness affect the required carbide grade, Modernstes Design, Flötenkonfiguration, Beschichtung, and overall tool structure.
General and Hardened Materials
For general machining below approximately HRC45, a general-purpose carbide ball nose series may be suitable.
For workpieces around HRC55–70, the high-hardness series uses ultrafine low-cobalt carbide, verstärkte Schneiden, a larger core, and multilayer nano-composite coatings. Selected custom designs can be evaluated for materials up to HRC75.
The final choice should still consider the cutter diameter, Bearbeitungszugabe, Maschinenzustand, und erforderliches Finish.
Aluminum and Copper
Aluminum and copper require different cutting conditions from hardened steel.
When selecting a cutter for these materials, prioritize suitable edge geometry, Spanabfuhr, and the correct material-specific tool configuration. Cutter size, Bearbeitungstiefe, and surface finish requirement should also be considered before confirming the tool.
Graphitelektroden
Graphite machining requires a dedicated wear-resistant tool solution. CutterBest’s graphite ball end mill series uses CVD diamond coating.
For dedicated graphite machining tools, siehe unsere Diamantbeschichtete Schaftfräser.
2. Choose by CNC Machining Purpose
The correct cutter also depends on whether the operation involves roughing, Halbfertigbearbeitung, or final finishing.
Schruppen und Vorschlichten
A ball nose cutter is generally not the first choice for heavy stock removal. In vielen Fällen, a flat or roughing end mill removes most of the material first.
A ball nose cutter can then machine curved areas, Radien, Hohlraumwände, and transitional surfaces during semi-finishing.
Final Finishing
For final finishing, surface quality becomes more important than material-removal rate.
Werkzeugsteifigkeit, suitable geometry, limited runout, correct reach, and a stable toolpath all affect the finished surface.
3D Konturfräsen
Ball nose end mills are well suited to slopes, Kurven, Freiformflächen, and complex 3D profiles because the rounded cutting end follows changing surface angles.
For a detailed applications guide, lesen Wofür wird ein Kugelkopffräser verwendet??
3. Choose by Diameter, Kugelradius, and Tool Reach
Diameter selection affects rigidity, detail resolution, Zugänglichkeit, und Bearbeitungseffizienz.
A smaller cutter can reach narrow cavities, small radii, und detaillierte Profile. A larger cutter generally provides greater rigidity and may machine broader curved surfaces more efficiently.
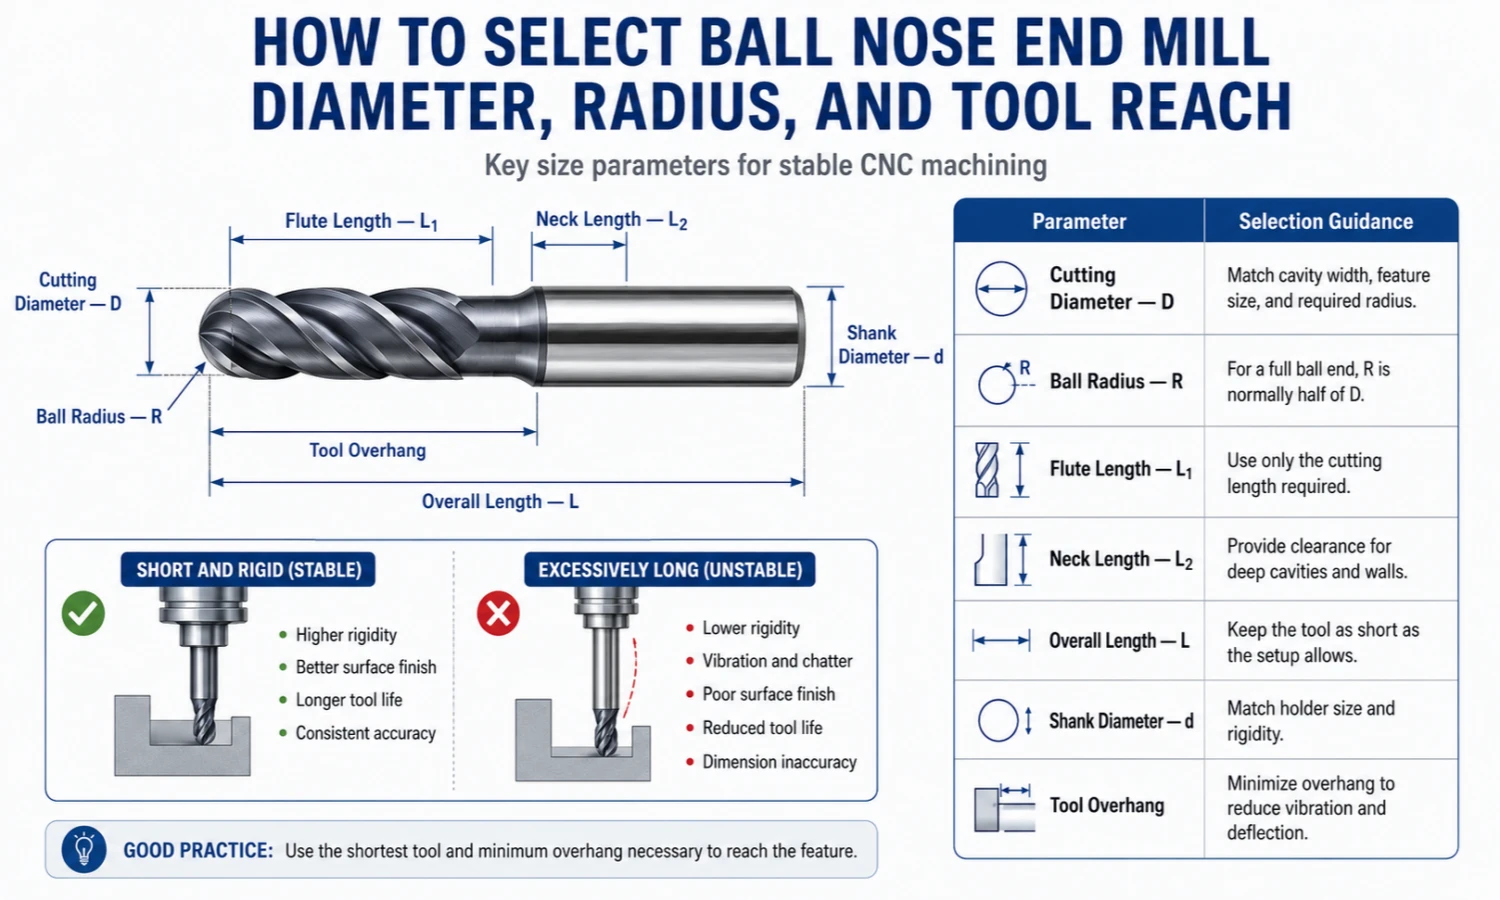
Für ein Standard-Vollkugelkopf-Design, Der Kugelradius beträgt normalerweise die Hälfte des Schneidendurchmessers.
Zum Beispiel:
- 4 mm cutting diameter normally corresponds to R2
- 6 mm cutting diameter normally corresponds to R3
- 10 mm cutting diameter normally corresponds to R5
The main dimensions to confirm are:
| Parameter | Auswahlpunkt |
|---|---|
| Cutting Diameter — D | Match the cavity width, feature size, and required radius |
| Ball Radius — R | For a full ball end, R is normally half of D |
| Flötenlänge | Use only the cutting length required for the operation |
| Halslänge | Provide sufficient clearance for deep cavities and walls |
| Gesamtlänge | Keep the tool as short as the setup allows |
| Schaftdurchmesser | Match the holder and required tool rigidity |
| Werkzeugüberhang | Minimize unnecessary overhang |
Schnittdurchmesser
Choose the diameter according to the part radius, Hohlraumbreite, feature size, verfügbaren Bearbeitungsraum, and required machining efficiency.
An unnecessarily small cutter may reduce rigidity and increase machining time, even if it can physically reach the feature.
Flute Length and Neck Length
Verwenden Sie nur die für den Schneidbereich erforderliche Nutlänge.
Für tiefe Hohlräume, neck clearance can be more important than simply increasing flute length. A relieved-neck or long-reach structure may provide access while maintaining greater cutter strength.
For dedicated deep-cavity tools, siehe unsere Kugelkopffräser mit großer Reichweite.
Overall Length and Overhang
Use the shortest practical overall length for the setup.
Excessive overhang can reduce rigidity and increase vibration or cutter deflection. Machine rigidity and workpiece clamping should also support the required reach.
4. Choose by Flute Count
Die Anzahl der Nuten beeinflusst den Spanraum, modernste Zählung, Steifigkeit, and surface-finish behavior.
CutterBest currently offers both 2-flute and 4-flute ball nose configurations.
2 Schaftfräser mit Kugelfräser
A 2-flute design provides larger chip channels and more chip space.
The suitable application still depends on the cutter diameter, Werkstückmaterial, Bearbeitungstiefe, and chip evacuation requirements.
4 Schaftfräser mit Kugelfräser
A 4-flute design provides more cutting edges and may be selected where additional edge count and cutter stability are useful.
The final configuration should match the material, Härte, Fräsergröße, Bearbeitungstiefe, und Endbearbeitungsanforderung.
Do not choose flute count only by habit. A 2-flute or 4-flute cutter should be selected as part of the complete tool configuration.
5. Choose by Coating and Edge Treatment
Coating should match the workpiece material, Härte, cutter series, und Bearbeitungsbedingungen.
For the confirmed CutterBest ball nose product range:
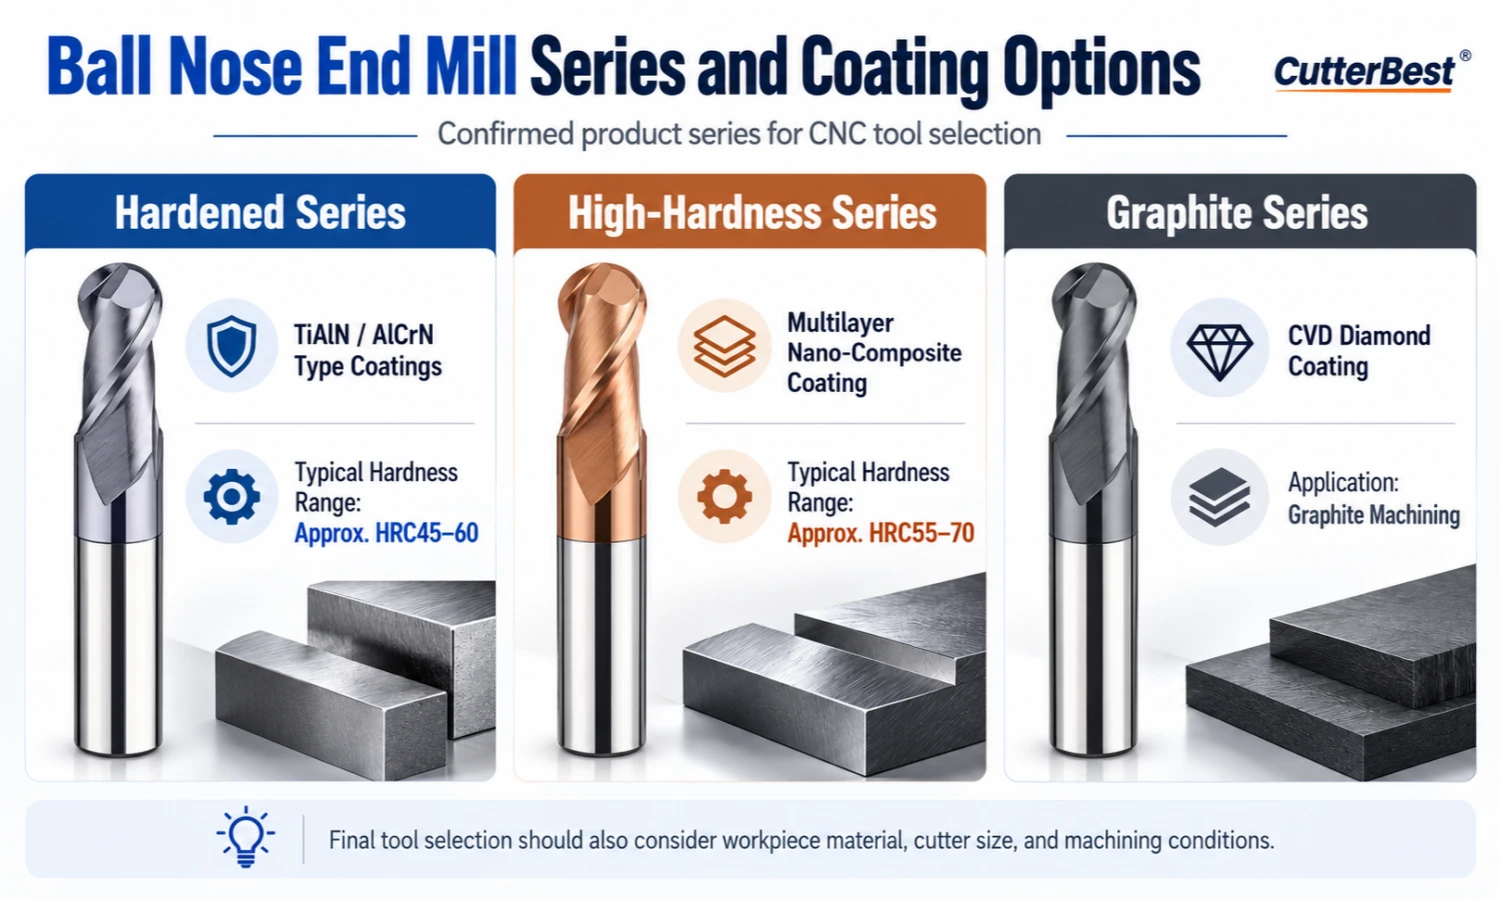
| Product Series | Confirmed Coating / Werkzeugstruktur |
|---|---|
| Hardened Series | TiAlN- oder AlCrN-Beschichtungen |
| High-Hardness Series | Multilayer nano-composite coatings with reinforced cutting edges and a larger core |
| Graphite Series | CVD diamond coating |
Coating should not be selected separately from the carbide grade, Modernstes Design, Flötenkonfiguration, und Werkstückmaterial.
Für Aluminium, Kupfer, and other specialized applications, confirm the appropriate tool configuration according to the actual workpiece and finishing requirement rather than choosing a coating name alone.
6. Choose by Surface Finish Requirement
Surface finish is one of the main reasons machinists use ball nose cutters, but the cutter itself does not determine the final result.
Important factors include:
- Programmed step-over
- Werkzeugwegrichtung
- Werkzeugunrundheit
- Cutter overhang
- Tool-holder condition
- Steifigkeit der Maschine
- Werkstückspannung
A smaller step-over can reduce scallop height, but it also increases the number of tool passes and machining time.
The center of a ball end also has a lower effective cutting speed than the outer cutting edge. Toolpath strategy and machine stability should therefore be considered together with the cutter specification.
7. Überprüfen Sie die Stabilität der Maschine und des Werkzeughalters
Even a correctly selected cutter may perform poorly in an unstable setup.
Before machining, check the tool holder, Auslaufen, Fräserüberstand, Spindelzustand, Werkstückspannung, and overall machine rigidity.
Use the shortest practical tool reach and maintain a clean, accurate holder connection.
If vibration occurs, review the complete setup rather than assuming the cutter itself is the only cause.
Ball Nose or Bull Nose End Mill?
A ball nose end mill has a fully rounded cutting end and is commonly used for 3D contours, gekrümmte Oberflächen, und Formhohlräume.
A bull nose end mill has a flat center with rounded corners and serves a different machining purpose.
Zum vollständigen Vergleich, lesen Bull-Schaft-Schaftfräser vs. Kugel-Schaftfräser.
Common Mistakes When Choosing a Ball Nose End Mill
Choosing the Wrong Cutter Series
Do not select a cutter based only on diameter. Workpiece material and hardness should match the appropriate general-purpose, gehärtet, hohe Härte, or specialized product series.
Verwendung eines zu großen Werkzeugüberhangs
Excessive overhang reduces rigidity and can increase vibration or cutter deflection. Use the shortest practical reach for the operation.
Ignoring Flute Count
A 2-flute and a 4-flute cutter have different flute-space and cutting-edge characteristics. Select the flute configuration according to the material, Fräsergröße, und Bearbeitungsanforderungen.
Ignoring Ball Radius and Neck Clearance
Cutting diameter alone does not define the complete cutter geometry. Kugelradius, Flötenlänge, Halsfreiheit, Schaftdurchmesser, and overall reach can all affect accessibility and rigidity.
Using a Ball Nose Cutter for Flat-Bottom Machining
A rounded cutting end does not efficiently create flat-bottom slots, Taschen, oder quadratische Schultern.
For these operations, siehe unsere Flacher Schaftfräser.
When Is a Custom Ball Nose End Mill Needed?
A custom cutter may be appropriate when a standard tool cannot provide the required radius, erreichen, Spielraum, Steifigkeit, oder Geometrie.
CutterBest can evaluate non-standard requirements from drawings, Größenangaben, vorhandene Werkzeugreferenzen, Werkstückmaterial, Härte, und Bearbeitungsbedingungen.
Für Standard- und kundenspezifische Produktoptionen, Sehen Sie sich unsere an Hartmetall-Kugelfräser.
Final Ball Nose End Mill Selection Checklist
Vor der Bestellung, bestätigen:
- Werkstückmaterial und Härte
- Bearbeitungsvorgang
- Cutting diameter and ball radius
- Required flute and neck length
- Tool reach and clearance
- 2-flute or 4-flute configuration
- Suitable coating or cutter series
- Anforderung an die Oberflächenbeschaffenheit
- Machine and holder stability
- Whether a standard or custom cutter is required
This information helps reduce specification errors and makes the quotation process more accurate.
If you are still deciding So wählen Sie einen Kugelkopffräser aus, Beginnen Sie mit dem Werkstückmaterial, Bearbeitungszweck, Fräsergröße, Flötenkonfiguration, und erforderliche Oberflächenbeschaffenheit.
Häufig gestellte Fragen
How do I choose a ball nose end mill?
Choose the cutter according to the workpiece material and hardness, Bearbeitungszweck, Schnittdurchmesser, Kugelradius, Flötenzahl, Beschichtung, Werkzeugreichweite, Anforderungen an die Oberflächenbeschaffenheit, und Maschinenstabilität.
Should I choose a 2-flute or 4-flute ball nose end mill?
The correct flute count depends on the material, Fräserdurchmesser, Bearbeitungstiefe, Spanabfuhr, Steifigkeit, und Endbearbeitungsanforderung. CutterBest offers both 2-flute and 4-flute configurations.
How do I select the correct ball radius?
For a standard full ball-end cutter, Der Kugelradius beträgt normalerweise die Hälfte des Schneidendurchmessers. The final radius should match the part geometry, Hohlraum, Profil, und erforderliche Oberflächenbeschaffenheit.
When should I request a custom ball nose end mill?
Consider a custom tool when a standard cutter cannot provide the required dimensions, Radius, erreichen, Spielraum, or other machining-specific geometry.
Senden Sie Ihre Anfrage für Kugelkopffräser
Need help selecting the correct ball nose end mill for your CNC application?
Sehen Sie sich unsere an Hartmetall-Kugelfräser for available product series and custom options.
Send your inquiry by email at sales@cutterbest.com, oder kontaktieren Sie uns unter WhatsApp.