 Cortadores de fresagem de precisão,Ferramentas de corte para usinagem CNC de todos os materiais

Entender como escolher uma fresa de topo esférica pode ajudar a melhorar o acabamento superficial, machining stability, and tool selection accuracy. No entanto, the correct cutter depends on more than diameter alone.
This guide explains how to select a ball nose end mill according to the workpiece material, finalidade de usinagem, diâmetro do cortador, raio da bola, contagem de flauta, coating or edge treatment, alcance da ferramenta, estabilidade da máquina, e exigência de acabamento superficial.
For available standard and custom carbide cutters, veja nosso Fresas de ponta esférica de metal duro.
Guia rápido de seleção de fresa de topo esférico
A tabela abaixo fornece um ponto de partida prático. Final tool selection should also consider the actual part geometry, dureza da peça, profundidade de usinagem, condição da máquina, e exigência de acabamento.
| Requisito de usinagem | Foco de seleção |
|---|---|
| Usinagem CNC Geral | Match the cutter series to the workpiece material and hardness |
| Materiais Endurecidos | Select the appropriate hardened or high-hardness series |
| Eletrodos de grafite | Use a dedicated graphite tool with CVD diamond coating |
| Cavidades Profundas | Confirm neck clearance, alcance da ferramenta, and minimum practical overhang |
| Detalhes 3D finos | Use a diameter and ball radius that match the feature size |
| 2-Flute or 4-Flute | Choose according to material, espaço para fichas, rigidez, and finishing requirements |
| Alto acabamento superficial | Control tool reach, acabar, step-over, e estabilidade da máquina |
This table is a starting point rather than a universal specification. The final cutter should match the actual workpiece and machining setup.
Por que escolher a fresa de topo esférica certa é importante
A ball nose end mill has a fully rounded cutting end that follows slopes, cáries, raios, and complex three-dimensional profiles.
No entanto, one cutter cannot suit every machining condition. Dureza da peça, tamanho do cortador, configuração de flauta, revestimento, alcance da ferramenta, and machine stability all affect the final result.
The purpose of tool selection is therefore not simply to choose a diameter. The complete cutter configuration should match the workpiece and machining requirement.
Como escolher uma fresa de topo esférico: 7 Fatores-chave
Antes de fazer o pedido, confirm these seven factors:
- Material e dureza da peça
- Finalidade de usinagem
- Diâmetro de corte, raio da bola, e alcance da ferramenta
- Contagem de flauta
- Revestimento ou tratamento de borda
- Requisito de acabamento de superfície
- Machine and tool-holder stability
Each factor affects the others, so they should be evaluated together.
1. Escolha por material da peça de trabalho
Workpiece material and hardness affect the required carbide grade, design de ponta, configuração de flauta, revestimento, and overall tool structure.
General and Hardened Materials
For general machining below approximately HRC45, a general-purpose carbide ball nose series may be suitable.
For workpieces around HRC55–70, the high-hardness series uses ultrafine low-cobalt carbide, reinforced cutting edges, a larger core, and multilayer nano-composite coatings. Selected custom designs can be evaluated for materials up to HRC75.
The final choice should still consider the cutter diameter, subsídio de usinagem, condição da máquina, e acabamento necessário.
Aluminum and Copper
Aluminum and copper require different cutting conditions from hardened steel.
When selecting a cutter for these materials, prioritize suitable edge geometry, evacuação de cavacos, and the correct material-specific tool configuration. Cutter size, profundidade de usinagem, and surface finish requirement should also be considered before confirming the tool.
Eletrodos de grafite
Graphite machining requires a dedicated wear-resistant tool solution. CutterBest’s graphite ball end mill series uses CVD diamond coating.
For dedicated graphite machining tools, veja nosso Fresas de topo revestidas de diamante.
2. Escolha por finalidade de usinagem CNC
The correct cutter also depends on whether the operation involves roughing, semi-acabamento, ou acabamento final.
Desbaste e Semiacabamento
Um cortador de ponta esférica geralmente não é a primeira escolha para remoção pesada de material. Em muitos casos, uma fresa de topo plana ou de desbaste remove a maior parte do material primeiro.
A ball nose cutter can then machine curved areas, raios, paredes da cavidade, and transitional surfaces during semi-finishing.
Acabamento Final
For final finishing, surface quality becomes more important than material-removal rate.
Rigidez da ferramenta, suitable geometry, esgotamento limitado, correct reach, and a stable toolpath all affect the finished surface.
3Fresamento de contorno D
Ball nose end mills are well suited to slopes, curvas, superfícies de forma livre, and complex 3D profiles because the rounded cutting end follows changing surface angles.
For a detailed applications guide, ler Para que é usada uma fresa de topo esférico?
3. Escolha por diâmetro, Raio da bola, e alcance da ferramenta
Diameter selection affects rigidity, resolução de detalhes, acessibilidade, e eficiência de usinagem.
Um cortador menor pode alcançar cavidades estreitas, raios pequenos, e perfis detalhados. A larger cutter generally provides greater rigidity and may machine broader curved surfaces more efficiently.
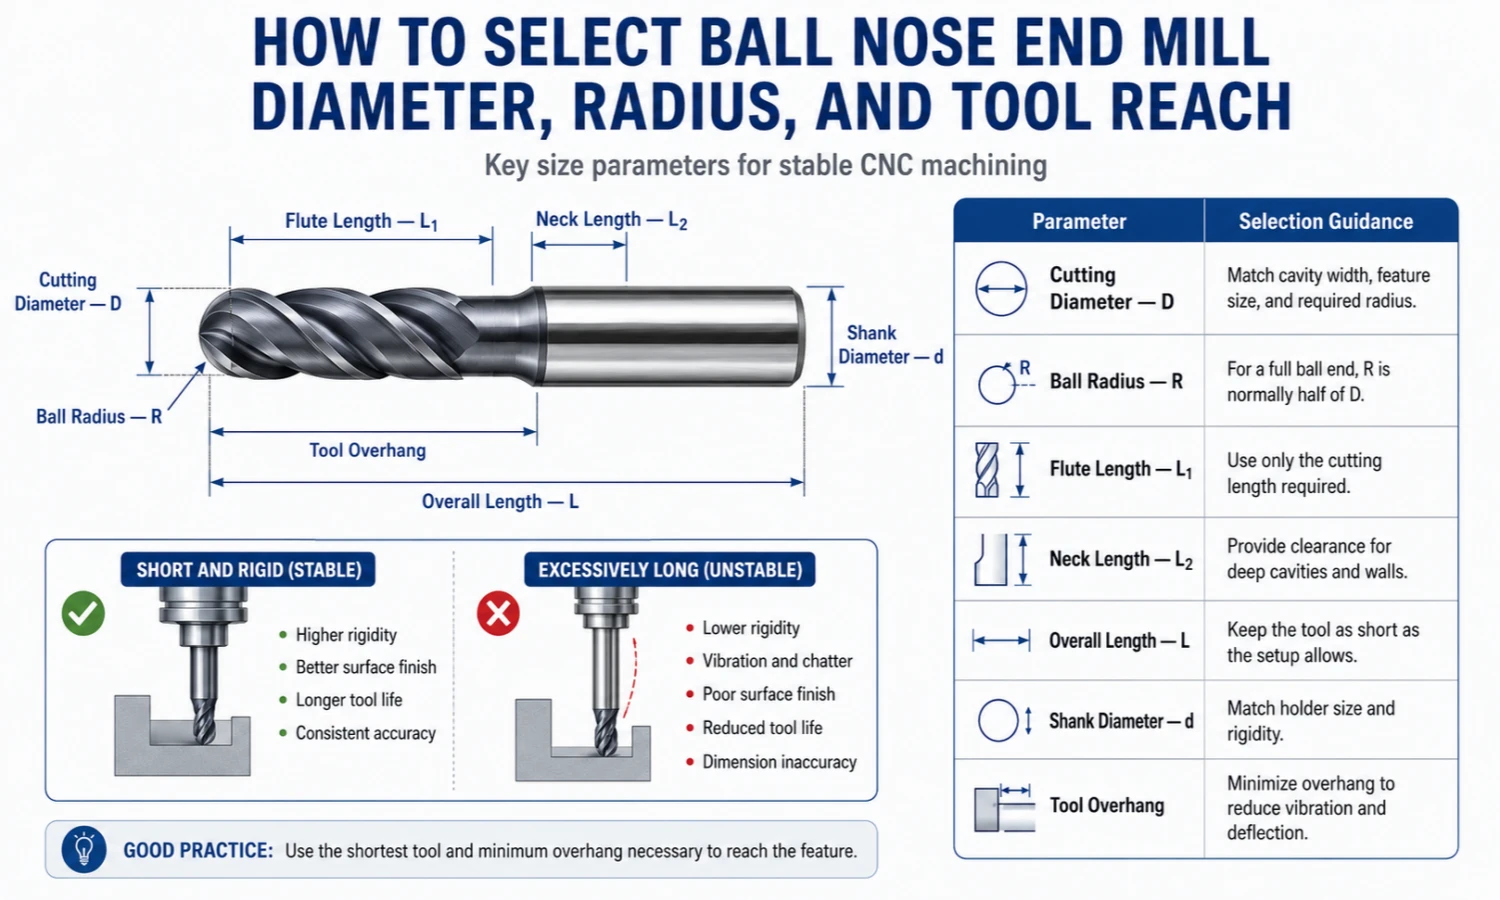
Para um design padrão de extremidade esférica completa, o raio da esfera é normalmente metade do diâmetro de corte.
Por exemplo:
- 4 mm de diâmetro de corte normalmente corresponde a R2
- 6 mm de diâmetro de corte normalmente corresponde a R3
- 10 mm de diâmetro de corte normalmente corresponde a R5
The main dimensions to confirm are:
| Parâmetro | Ponto de seleção |
|---|---|
| Diâmetro de corte — D | Combine a largura da cavidade, tamanho do recurso, e raio necessário |
| Raio da esfera — R | Para um final de bola completo, R normalmente é metade de D |
| Comprimento da Flauta | Use apenas o comprimento de corte necessário para a operação |
| Comprimento do pescoço | Provide sufficient clearance for deep cavities and walls |
| Comprimento total | Mantenha a ferramenta tão curta quanto a configuração permitir |
| Diâmetro da haste | Match the holder and required tool rigidity |
| Saliência da ferramenta | Minimize unnecessary overhang |
Diâmetro de corte
Choose the diameter according to the part radius, cavity width, tamanho do recurso, espaço de usinagem disponível, e eficiência de usinagem necessária.
An unnecessarily small cutter may reduce rigidity and increase machining time, even if it can physically reach the feature.
Comprimento da flauta e comprimento do pescoço
Use only the flute length required for the cutting area.
Para cavidades profundas, neck clearance can be more important than simply increasing flute length. A relieved-neck or long-reach structure may provide access while maintaining greater cutter strength.
For dedicated deep-cavity tools, veja nosso Fresa de topo esférico de longo alcance.
Overall Length and Overhang
Use the shortest practical overall length for the setup.
Excessive overhang can reduce rigidity and increase vibration or cutter deflection. Machine rigidity and workpiece clamping should also support the required reach.
4. Choose by Flute Count
Flute count affects chip space, contagem de ponta, rigidez, and surface-finish behavior.
CutterBest currently offers both 2-flute and 4-flute ball nose configurations.
2 Fresas de ponta esférica de flauta
A 2-flute design provides larger chip channels and more chip space.
The suitable application still depends on the cutter diameter, material da peça, profundidade de usinagem, and chip evacuation requirements.
4 Fresas de ponta esférica de flauta
A 4-flute design provides more cutting edges and may be selected where additional edge count and cutter stability are useful.
The final configuration should match the material, dureza, tamanho do cortador, profundidade de usinagem, e exigência de acabamento.
Do not choose flute count only by habit. A 2-flute or 4-flute cutter should be selected as part of the complete tool configuration.
5. Escolha por revestimento e tratamento de borda
Coating should match the workpiece material, dureza, cutter series, e condições de usinagem.
For the confirmed CutterBest ball nose product range:
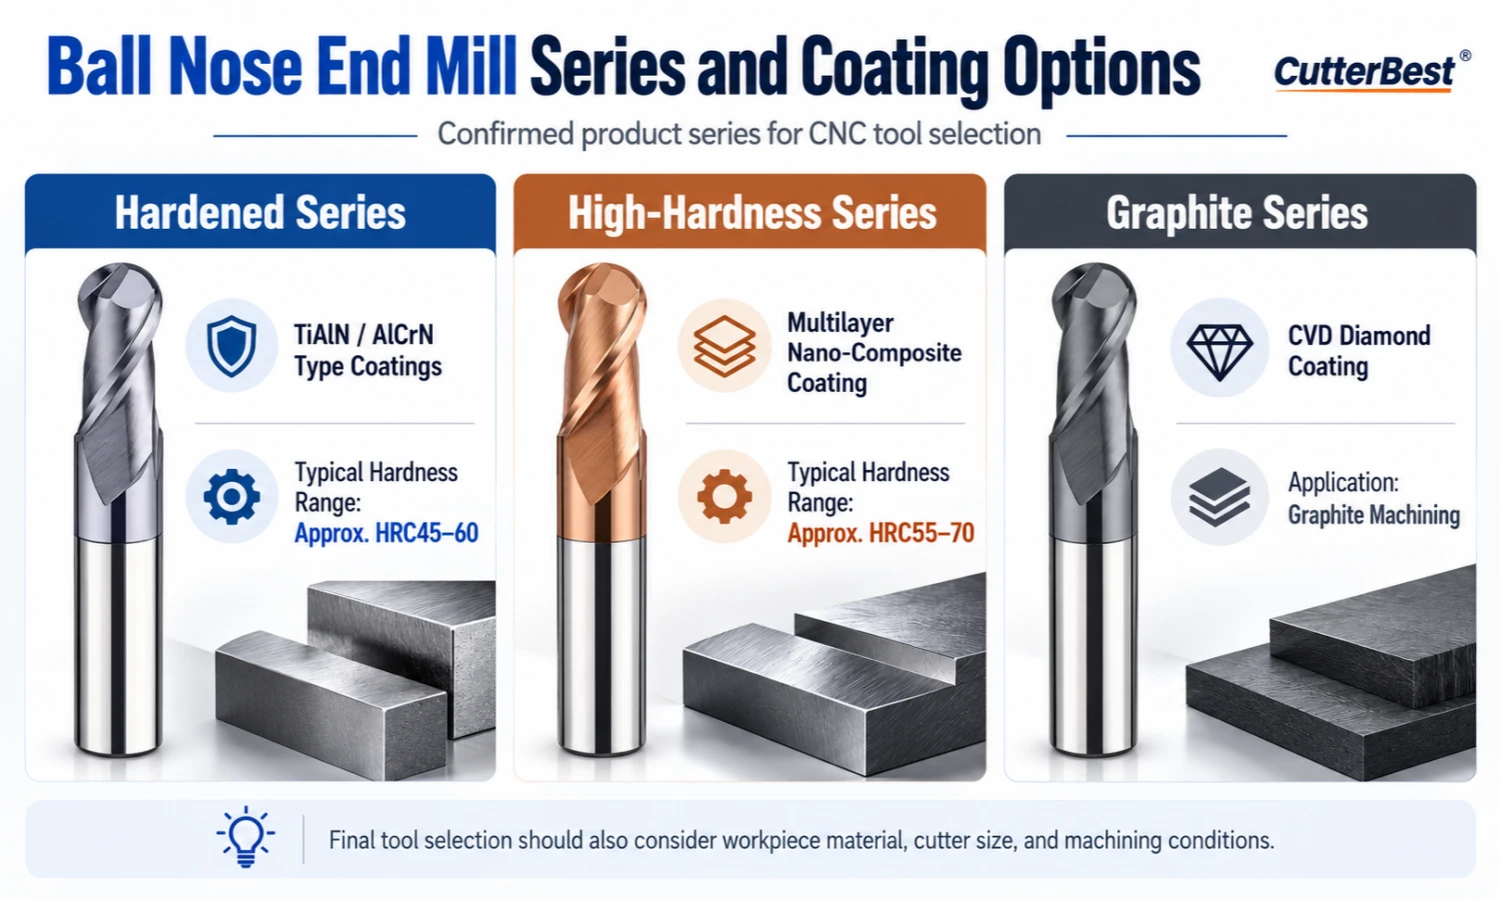
| Product Series | Confirmed Coating / Estrutura da ferramenta |
|---|---|
| Hardened Series | TiAlN- or AlCrN-type coatings |
| High-Hardness Series | Multilayer nano-composite coatings with reinforced cutting edges and a larger core |
| Graphite Series | Revestimento de diamante CVD |
Coating should not be selected separately from the carbide grade, design de ponta, configuração de flauta, e material da peça.
Para alumínio, cobre, and other specialized applications, confirm the appropriate tool configuration according to the actual workpiece and finishing requirement rather than choosing a coating name alone.
6. Escolha por requisito de acabamento de superfície
Surface finish is one of the main reasons machinists use ball nose cutters, but the cutter itself does not determine the final result.
Important factors include:
- Passo a passo programado
- Direção do percurso
- Excentricidade da ferramenta
- Saliência do cortador
- Condição do porta-ferramenta
- Rigidez da máquina
- Fixação da peça
A smaller step-over can reduce scallop height, but it also increases the number of tool passes and machining time.
The center of a ball end also has a lower effective cutting speed than the outer cutting edge. Toolpath strategy and machine stability should therefore be considered together with the cutter specification.
7. Verifique a estabilidade da máquina e do porta-ferramentas
Mesmo uma fresa selecionada corretamente pode ter um desempenho ruim em uma configuração instável.
Antes da usinagem, check the tool holder, acabar, cutter overhang, condição do fuso, fixação de peças, and overall machine rigidity.
Use o menor alcance prático da ferramenta e mantenha uma limpeza, conexão precisa do suporte.
Se ocorrer vibração, review the complete setup rather than assuming the cutter itself is the only cause.
Ball Nose or Bull Nose End Mill?
A ball nose end mill has a fully rounded cutting end and is commonly used for 3D contours, superfícies curvas, e cavidades de molde.
A bull nose end mill has a flat center with rounded corners and serves a different machining purpose.
For the complete comparison, ler Fresa de topo Bull Nose vs Fresa de topo Ball Nose.
Erros comuns ao escolher uma fresa de topo esférico
Choosing the Wrong Cutter Series
Do not select a cutter based only on diameter. Workpiece material and hardness should match the appropriate general-purpose, endurecido, high-hardness, or specialized product series.
Usando muita saliência da ferramenta
Excessive overhang reduces rigidity and can increase vibration or cutter deflection. Use the shortest practical reach for the operation.
Ignorando a contagem de flautas
A 2-flute and a 4-flute cutter have different flute-space and cutting-edge characteristics. Select the flute configuration according to the material, tamanho do cortador, e exigência de usinagem.
Ignorando o raio da bola e a folga do pescoço
Cutting diameter alone does not define the complete cutter geometry. Raio da bola, comprimento da flauta, folga do pescoço, diâmetro da haste, and overall reach can all affect accessibility and rigidity.
Usando um cortador de ponta esférica para usinagem de fundo plano
A rounded cutting end does not efficiently create flat-bottom slots, bolsos, ou ombros quadrados.
Para estas operações, veja nosso Fresa de topo plano.
When Is a Custom Ball Nose End Mill Needed?
A custom cutter may be appropriate when a standard tool cannot provide the required radius, alcançar, liberação, rigidez, ou geometria.
CutterBest can evaluate non-standard requirements from drawings, size information, referências de ferramentas existentes, material da peça, dureza, e condições de usinagem.
For standard and custom product options, veja nosso Fresas de ponta esférica de metal duro.
Final Ball Nose End Mill Selection Checklist
Antes de fazer o pedido, confirmar:
- Material e dureza da peça
- Operação de usinagem
- Diâmetro de corte e raio da esfera
- Required flute and neck length
- Tool reach and clearance
- 2-flute or 4-flute configuration
- Suitable coating or cutter series
- Requisito de acabamento de superfície
- Machine and holder stability
- Whether a standard or custom cutter is required
This information helps reduce specification errors and makes the quotation process more accurate.
If you are still deciding como escolher uma fresa de topo esférica, comece com o material da peça de trabalho, finalidade de usinagem, tamanho do cortador, configuração de flauta, e acabamento superficial necessário.
Perguntas frequentes
Como escolho uma fresa de topo esférica?
Choose the cutter according to the workpiece material and hardness, finalidade de usinagem, diâmetro de corte, raio da bola, contagem de flauta, revestimento, alcance da ferramenta, exigência de acabamento superficial, e estabilidade da máquina.
Should I choose a 2-flute or 4-flute ball nose end mill?
The correct flute count depends on the material, diâmetro do cortador, profundidade de usinagem, evacuação de cavacos, rigidez, e exigência de acabamento. CutterBest offers both 2-flute and 4-flute configurations.
Como seleciono o raio correto da bola?
Para um cortador de ponta esférica padrão, o raio da esfera é normalmente metade do diâmetro de corte. The final radius should match the part geometry, cavidade, perfil, e acabamento superficial necessário.
When should I request a custom ball nose end mill?
Consider a custom tool when a standard cutter cannot provide the required dimensions, raio, alcançar, liberação, or other machining-specific geometry.
Send Your Ball Nose End Mill Inquiry
Need help selecting the correct ball nose end mill for your CNC application?
Veja nosso Fresas de ponta esférica de metal duro para séries de produtos disponíveis e opções personalizadas.
Envie sua consulta por e-mail para vendas@cutterbest.com, ou entre em contato conosco em WhatsApp.