 Precision Milling Cutters,Cutting Tools for CNC Machining Every Material
When comparing a 2 flute vs 3 flute end mill for aluminum, start with the machining operation.
Choose a 2-flute end mill when deep slotting, heavy roughing, or high chip volume makes chip evacuation the main concern. Its larger flute spaces give aluminum chips more room to leave the cutting area.
Choose a 3-flute end mill when side-wall quality, profile stability, semi-finishing, or finishing matters more. The additional cutting edge can provide more consistent engagement and better rigidity in a comparable cutter design.
Neither flute count suits every aluminum job. Slot depth, radial engagement, tool reach, holder condition, coolant or air blast, toolpath, and surface requirements can change the final choice.
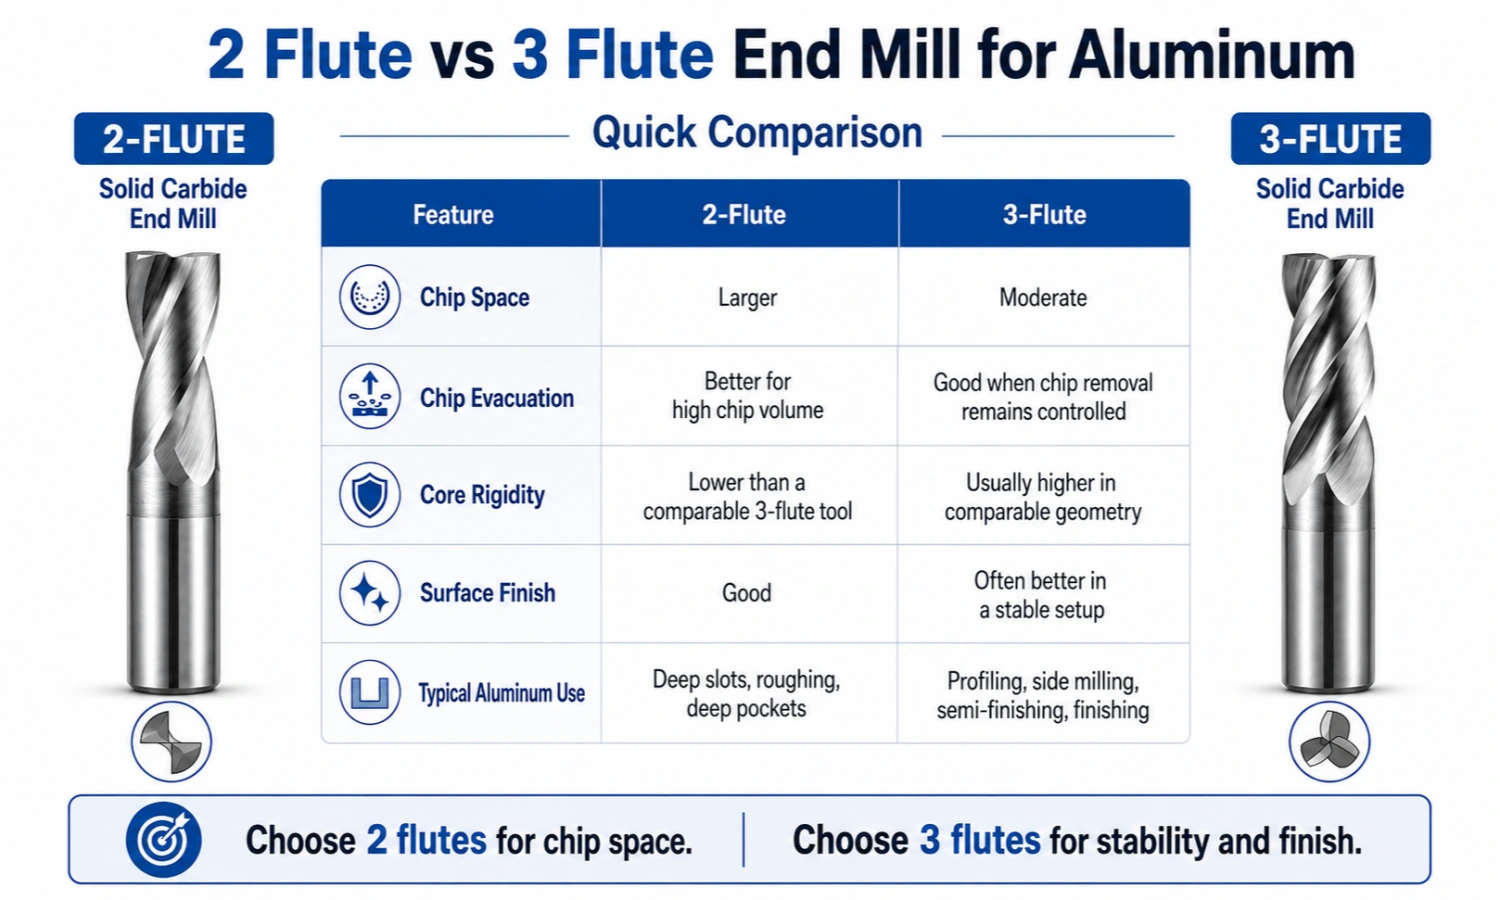
Quick Comparison: 2 Flute vs 3 Flute End Mill for Aluminum
| Selection Factor | 2-Flute End Mill | 3-Flute End Mill |
|---|---|---|
| Chip Space | Larger | Moderate |
| Chip Evacuation | Better for high chip volume | Good when chip removal remains controlled |
| Core Rigidity | Lower than a comparable 3-flute tool | Usually higher in comparable geometry |
| Deep Full-Width Slotting | Usually preferred | Suitable under controlled conditions |
| Heavy Roughing | Usually preferred | Better for moderate removal |
| Side Milling | Suitable | Often preferred |
| Surface Finish | Good | Often better in a stable setup |
| Typical Aluminum Use | Deep slots, roughing, deep pockets | Profiling, side milling, semi-finishing, finishing |
Choose 2 flutes when chip space and safe chip removal are the priorities. Choose 3 flutes when cutting stability, side-wall quality, and finishing potential matter more.
These are starting recommendations, not fixed rules. The complete machining setup still affects the result.
Why Flute Count Matters in Aluminum Machining
Chip Space and Chip Evacuation
Aluminum often produces large, soft, or continuous chips. When these chips remain inside a slot or pocket, the cutter may recut them. Chips may also stick to the cutting edge or scratch the machined surface.
A 2-flute end mill provides larger flute spaces. It normally handles high chip volume more easily than a comparable 3-flute cutter.
This advantage becomes important in deep full-width slots and enclosed pockets, where chips have limited room to escape.
A 3-flute tool still provides useful chip space. However, the toolpath, coolant, air blast, and cutting engagement must help chips leave the cutting zone.
Core Rigidity and Tool Deflection
In comparable designs, a 3-flute cutter often has more core material than a 2-flute cutter. The stronger core can reduce tool deflection during side milling and profiling.
Lower deflection helps the cutter maintain a more consistent wall position. It may also improve profile accuracy and reduce visible wall variation.
Flute count cannot correct a weak setup. Excessive tool reach, holder runout, poor clamping, or unstable machine conditions can still cause chatter and dimensional changes.
Use the shortest practical tool length and stable tool holding before relying on flute count to improve the result.
Cutting-Edge Engagement and Surface Finish
A 3-flute end mill creates three cutting engagements per revolution instead of two.
Under stable conditions, the additional engagement can support smoother side walls and a more consistent finish. This is one reason three-flute cutters are often selected for profiling, semi-finishing, and finishing.
The final surface also depends on:
- Feed per tooth
- Tool runout
- Edge geometry
- Tool wear
- Holder condition
- Machine rigidity
- Radial engagement
- Coolant or air delivery
A higher flute count may improve finishing potential, but it does not guarantee a specific surface result.
When to Choose a 2-Flute End Mill for Aluminum
Deep Full-Width Slotting
Choose a 2-flute end mill when the slot is deep, full-width engagement is required, and chips have limited room to escape.
During full-width slotting, both sides of the cutter remain engaged with the material. Chips must travel through the flutes before leaving the slot.
A two-flute design provides more room for chip flow. It is usually the safer starting choice when chip packing presents a higher risk.
Coolant or air blast remains important. A 2-flute cutter cannot compensate for excessive engagement or poor chip removal.
Heavy Roughing and High Chip Volume
Choose 2 flutes when high chip volume and safe chip evacuation matter more than final wall finish.
Heavy roughing removes more material and produces more chips. Larger flute spaces can reduce the risk of chip recutting and flute blockage.
The cutter must still match the machine, holder, tool length, and cutting load. Excessive engagement can overload any cutter.
Deep Pocket Milling
Deep and enclosed pockets can trap chips around the tool. A 2-flute end mill is often a practical starting choice for these conditions.
A ramping entry, helical entry, or adaptive toolpath can reduce cutting engagement. Strong air blast or coolant can also move chips away from the bottom of the pocket.
For deep slotting, roughing, and high chip-volume aluminum machining, view our 2 Flute End Mill.
When to Choose a 3-Flute End Mill for Aluminum
Side Milling and Profiling
Choose a 3-flute end mill when stable side cutting and consistent wall quality matter more than maximum flute space.
During side milling, only part of the cutter diameter may contact the workpiece. Chip evacuation is often easier than it is during full-width slotting.
The third cutting edge can provide more consistent engagement during straight-wall milling, external profiling, internal contouring, and edge finishing.
Semi-Finishing and Finishing
Choose 3 flutes when surface consistency and side-wall finish are the main goals.
A three-flute tool can provide smoother engagement than some 2-flute cutters. It works best when the machine setup remains stable and tool overhang stays under control.
A 3-flute cutter will not automatically correct:
- Excessive runout
- Worn cutting edges
- Poor clamping
- Unstable feed
- Excessive tool reach
- Incorrect radial engagement
Check these conditions before changing the flute count.
Controlled Slotting and Pocketing
A 3-flute end mill can handle shallow or controlled slotting when the toolpath and chip evacuation are suitable.
Lighter engagement, staged cutting, a ramping entry, a helical entry, or an adaptive toolpath can reduce the amount of material engaged at one time.
For deeper full-width slots or heavy roughing, start with a 2-flute tool. The larger flute spaces provide a wider margin for chip removal.
For side milling, profiling, semi-finishing, and finishing, view our 3 Flute Carbide Flat End Mill for Aluminum.
For more details about three-flute applications, read our three-flute cutter application guide.
Decision Rules: 2 Flute or 3 Flute for Aluminum?
Rule 1: Start with Chip Volume and Slot Access
Start with a 2-flute cutter when:
- The slot is deep
- Full-width engagement is required
- The pocket is enclosed
- Chips have limited space to escape
- High chip volume is expected
A 3-flute cutter becomes more practical when the cutting area is open and the toolpath allows chips to leave freely.
Rule 2: Define the Main Machining Goal
Choose 2 flutes when material removal and chip evacuation are the priorities.
Choose 3 flutes when the operation focuses on:
- Side-wall quality
- Profile consistency
- Semi-finishing
- Finishing
- Stable side cutting
The primary machining goal should guide the starting choice.
Rule 3: Review Tool Reach and Setup Rigidity
Long tool reach increases deflection risk. Use the shortest practical tool and improve clamping before changing the flute count.
Do not use additional flutes as a substitute for stable tool holding.
If the setup remains weak, a 3-flute cutter may still vibrate or produce inconsistent dimensions. Review holder runout, tool reach, radial engagement, and machine rigidity together.
Rule 4: Check Coolant, Air Blast, and Toolpath
Flute count is only one part of chip control.
Strong air blast, suitable coolant delivery, and a toolpath that avoids excessive engagement can improve chip evacuation. These conditions may allow a 3-flute cutter to complete controlled slotting successfully.
If chips continue to collect, reduce engagement, improve chip removal, or move to a 2-flute tool.
Rule 5: Match Edge Geometry and Surface Treatment
Aluminum machining generally benefits from sharp cutting edges and smooth chip flow.
The cutter geometry and surface treatment should match:
- Aluminum grade
- Machining operation
- Coolant method
- Chip-adhesion risk
- Required tool life
- Surface requirement
Do not choose a cutter only by flute count or coating name. The complete tool design must match the application.
Recommended Flute Count by Aluminum Operation
| Aluminum Operation | Recommended Starting Choice | Main Reason |
|---|---|---|
| Deep full-width slotting | 2 Flutes | More chip space |
| Heavy roughing | 2 Flutes | Better chip evacuation |
| Deep pocket milling | 2 Flutes | Easier chip removal |
| Shallow controlled slotting | 2 or 3 Flutes | Depends on depth and chip control |
| Side milling | 3 Flutes | Better stability and wall quality |
| Profile and contour milling | 3 Flutes | More consistent engagement |
| Semi-finishing | 3 Flutes | Balanced chip space and rigidity |
| Finishing | 3 Flutes | Better finishing potential |
These are starting choices rather than absolute rules. Tool diameter, flute length, overall reach, machine rigidity, coolant, and cutting strategy can change the final decision.

Signs Your Flute Count or Setup May Be Wrong
| Observable Problem | Possible Cause | Practical Response |
|---|---|---|
| Chips pack inside the slot | Insufficient flute space or weak chip removal | Improve air or coolant, reduce engagement, or consider 2 flutes |
| Chips are recut and scratch the surface | Chips remain in the cutting zone | Adjust the toolpath and improve chip evacuation |
| Aluminum sticks to the cutting edge | Poor chip removal, worn edge, or unsuitable surface treatment | Check lubrication, edge condition, and flute surface |
| Side walls show chatter marks | Excessive reach, weak clamping, or unstable engagement | Shorten overhang and improve rigidity |
| Dimensions vary during profiling | Tool deflection or runout | Check the holder, runout, cutting load, and tool reach |
| Finish remains inconsistent | The setup or parameters are unstable | Review the complete cutting system before changing flute count |
These problems do not always mean that the flute count is wrong.
Changing from 2 flutes to 3 flutes will not correct excessive runout. Likewise, moving to 2 flutes will not solve weak coolant delivery if chips remain trapped inside a pocket.
Start with the visible problem. Check chip flow, tool reach, clamping, cutting load, and tool condition before selecting another cutter.
Common Mistakes When Selecting an Aluminum End Mill
Choosing by Flute Count Alone
Flute count does not fully describe a cutter.
Two tools with the same number of flutes may use different core sizes, flute depths, edge geometries, lengths, and surface treatments.
Compare the complete tool design and machining conditions.
Using More Flutes to Compensate for a Weak Setup
More flutes may improve rigidity in comparable cutter designs. However, they cannot repair a weak holder, excessive runout, poor clamping, or excessive tool overhang.
Fix the setup first. Then select the flute count according to chip volume and surface requirements.
Treating Recommendations as Absolute Rules
A 3-flute cutter can machine slots, and a 2-flute cutter can finish aluminum.
The recommendations in this guide describe practical starting choices:
- 2 flutes for more chip space
- 3 flutes for more stable engagement and better finishing potential
The final result depends on the complete machining setup.
Frequently Asked Questions
Is 2 Flute or 3 Flute Better for Aluminum?
A 2-flute end mill is usually better for deep slotting, heavy roughing, and operations where maximum chip space is required.
A 3-flute end mill is often better for side milling, profiling, semi-finishing, and finishing when cutting stability and wall quality matter more.
Is a 3-Flute End Mill Good for Aluminum Slotting?
Yes. A 3-flute cutter can work for shallow or controlled aluminum slotting when chip evacuation remains effective.
For deeper full-width slots or heavy roughing, a 2-flute cutter is usually the safer starting choice.
Which End Mill Gives a Better Finish in Aluminum?
A 3-flute end mill often provides better finishing potential because it creates more cutting engagements per revolution and may offer better rigidity.
Runout, feed, tool wear, clamping, machine stability, and radial engagement also affect the final surface.
Can a 2-Flute End Mill Be Used for Finishing Aluminum?
Yes. A sharp, stable 2-flute cutter can finish aluminum.
When side-wall consistency and surface finish are the priorities, a 3-flute cutter is often the better starting choice.
Need Help Choosing Between 2 and 3 Flutes?
Choosing between 2 and 3 flutes depends on the aluminum grade, machining operation, slot depth, tool reach, chip-control method, and required surface finish.
Send us the workpiece material, required dimensions, slot or pocket depth, quantity, and any available drawing or current cutter information.
Not sure which flute count to choose? Email your requirements to sales@cutterbest.com, and we will review whether a 2-flute or 3-flute tool better matches the application.