 Precision Milling Cutters,Cutting Tools for CNC Machining Every Material
Introduction
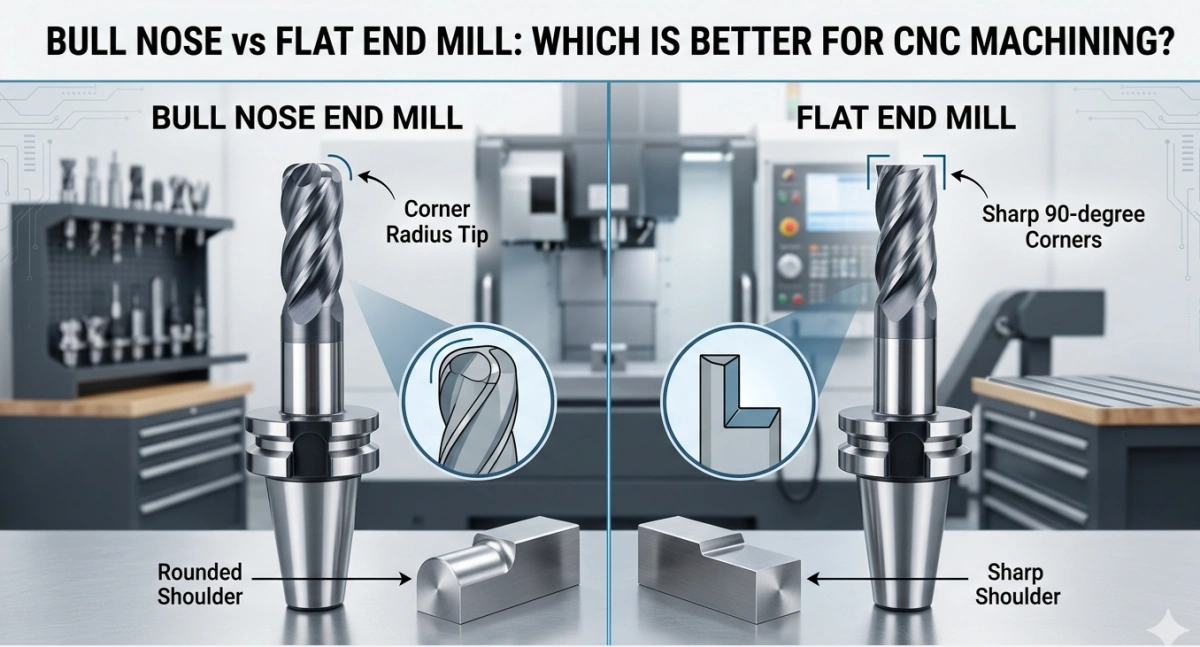
The bull nose vs flat end mill comparison mainly comes down to cutting-corner geometry. Both cutters can machine flat-bottom features, but a bull nose end mill has a defined corner radius, while a flat end mill has a sharp cutting corner.
That difference affects the geometry left on the finished part. If the drawing allows or specifies a radiused transition, a bull nose end mill may be the better match. If the feature requires a sharp 90-degree internal corner or square shoulder, a flat end mill is usually the more direct choice.
The correct selection therefore depends on the drawing, feature geometry, required corner condition, tool access, and tolerance rather than on one cutter being universally “better.”
Quick Answer: Bull Nose vs Flat End Mill
Choose a bull nose end mill when the feature allows or requires a corner radius or radiused bottom-to-wall transition.
Choose a flat end mill when the drawing requires a sharp 90-degree internal corner, square shoulder, or sharp lower corner.
A part that contains both radiused transitions and sharp square features may require both cutter geometries in different operations.
Bull Nose vs Flat End Mill: Key Differences
The table below compares the feature geometry each cutter is intended to produce. Actual cutter selection also depends on the drawing, available tool diameter, tolerance, feature accessibility, and machining setup.
| Comparison Point | Bull Nose / Corner Radius End Mill | Flat / Square End Mill |
|---|---|---|
| Cutting Corner | Flat bottom with a corner radius | Flat bottom with a sharp cutting corner |
| Bottom Geometry | Flat bottom with a radiused bottom-to-wall transition | Flat bottom with a sharp bottom-to-wall transition |
| Internal Corner Result | Leaves or follows a radiused internal transition | Used where a sharp 90-degree internal corner is required |
| Square Shoulder | Not suitable when the shoulder must remain sharp | Suitable when a sharp square shoulder is required |
| Slots / Square Features | Use when the feature allows a radius at the lower corners | Suitable where the feature requires sharp lower corners |
| Corner Condition on Drawing | Use when a radius is allowed or specified | Use when a sharp corner is required |
| Main Selection Trigger | Required radiused transition | Required sharp 90-degree corner or square shoulder |
How Corner Geometry Changes the Machined Feature

A bull nose end mill has a flat cutting bottom with a corner radius between the bottom cutting edge and the side cutting edge. As a result, the machined feature reflects a radiused transition rather than a sharp lower corner.
A flat end mill also has a flat cutting bottom, but its cutting corner is sharp rather than radiused. This geometry is used when the part drawing calls for a sharp internal corner, square shoulder, or other feature that does not allow a specified corner radius.
This distinction is more important than simply asking which cutter is stronger or more durable. The cutter should match the required geometry on the finished part.
A flat end mill also does not guarantee a mathematically perfect zero-radius internal corner in every situation. Tool diameter, cutter condition, toolpath, accessibility, and drawing tolerance can all affect the final feature.
Which End Mill Should You Choose?
Choose a Bull Nose End Mill When
A bull nose end mill is generally the more suitable geometry when:
- The drawing allows or specifies a corner radius
- The feature requires a radiused bottom-to-wall transition
- A stepped or shoulder feature allows a radius at the lower corner
- The required geometry combines a flat bottom with radiused corners
- A sharp 90-degree lower corner is not required
The cutter diameter, corner radius, reach, and other dimensions must still match the part geometry.
For available dimensions and configurations, see Bull Nose End Mill.
Choose a Flat End Mill When
A flat end mill is generally the more direct choice when:
- The drawing requires a sharp 90-degree internal corner
- A square shoulder must remain sharp
- A slot or square-bottom feature requires sharp lower corners
- The feature does not allow a corner radius
- The part geometry specifically calls for a sharp-corner flat-bottom cutter
The achievable corner still depends on cutter diameter, tool access, toolpath, and tolerance.
For available configurations, see Flat End Mill.
When Both Tools May Be Used
Some parts contain both radiused transitions and sharp square features. In those cases, different cutter geometries may be used for different features or machining stages.
This should not be treated as one fixed roughing or finishing sequence. The actual process depends on the drawing, stock allowance, tolerance, accessibility, and CAM strategy.
Bull Nose / Corner Radius vs Flat / Square Terminology
Tool names can vary between catalogs, regions, and suppliers.
The term bull nose end mill commonly describes a flat-bottom end mill with a corner radius, while corner radius end mill is another widely used catalog term for this geometry.
Likewise, flat end mill and square end mill are commonly used for sharp-corner, flat-bottom end mill profiles.
Therefore, searches such as corner radius vs square end mill, corner radius end mill vs flat end mill, and bull nose vs square end mill often refer to the same basic comparison covered on this page: a radiused cutting corner versus a sharp cutting corner.
These naming conventions can vary between manufacturers, so the final tool should always be confirmed by its actual geometry and dimensions.
Related Tool Comparisons
This page compares a corner-radius flat-bottom cutter with a sharp-corner flat-bottom cutter.
If you need to compare a bull nose cutter with a fully rounded cutting end, see Bull Nose End Mill vs Ball Nose End Mill.
For product specifications and custom configurations, see our Bull Nose End Mill and Flat End Mill product pages.
FAQ
What is the main difference between a bull nose and flat end mill?
Both cutters can have a flat cutting bottom. The main difference is the cutting corner. A bull nose end mill has a corner radius, while a flat end mill has a sharp cutting corner.
Which end mill should I use for a sharp internal corner?
Use a flat or square end mill when the drawing requires a sharp 90-degree internal corner or square shoulder.
The actual achievable corner also depends on cutter diameter, tool access, toolpath, and tolerance.
Which end mill should I use when a corner radius is allowed or required?
A bull nose or corner radius end mill is usually the more direct choice when the drawing allows or specifies a radiused transition at the bottom or shoulder of the feature.
The required R value should be confirmed from the drawing or machining requirement.
Can a bull nose end mill replace a flat end mill?
Not when the finished feature requires a sharp corner that does not allow a radius.
The two cutters can overlap in some machining operations, but their cutting corners produce different feature geometry.
Is corner radius vs square end mill the same comparison?
It is a closely related comparison. In many tooling catalogs, bull nose and corner radius refer to flat-bottom cutters with radiused corners, while flat and square end mill refer to sharp-corner flat-bottom profiles.
Naming varies between manufacturers, so the actual cutter geometry should still be confirmed.
Conclusion
The main difference between a bull nose and flat end mill is the required corner geometry on the finished part. Choose a bull nose or corner radius end mill when the drawing allows or specifies a radiused transition, and choose a flat or square end mill when a sharp 90-degree corner or square shoulder is required.
If you are unsure which geometry matches your part, send your drawing, critical feature dimensions, and machining requirements to us by email or contact us directly on WhatsApp for review.